Coating Diameter Control: Precision on the Secondary Line

Unexpected fact: By October 2023 this initiative touched 151 countries, covering roughly $41 trillion in GDP and about 5.1 billion people — a scale that redirected global trade routes. The term “facilities connectivity” here means how Beijing funded and built cross-border systems: ports, rail, and digital links that knit regions together. This intro outlines what was aimed for between 2013 and 2023, what got built, and where controversies rose.
Belt and Road Facilities Connectivity
Expect a short trend review: the early megaproject push, then a shift toward greener, smaller, and more digital initiatives. We will track policy tools, corridor planning, funding patterns, and the main beneficiaries.

This piece weighs the key tension: infrastructure as a development opportunity versus concerns about debt, governance, and geopolitics. Case studies include CPEC/Gwadar, Indonesia’s high-speed rail, and the Port of Piraeus to ground the analysis.

Belt And Road Facilities Connectivity In Context: What The Belt And Road Initiative Aimed To Do

When Xi Jinping launched the New Silk Road in 2013, he repositioned infrastructure as a tool for shared growth across continents.

Origins And The New Silk Road Framing

President Jinping used the silk road label to build legitimacy and win partner buy-in. The name helped rebrand many national plans as a single global program.

Scale And Reach By October 2023

By October 2023 the belt road initiative touched 151 countries, covered about $41 trillion in combined GDP, and linked roughly 5.1 billion people. This size made the belt road effort a system-level force, not a regional push.

Why “Connectivity” Became The Umbrella Goal

Connectivity grouped transport, energy, communications, investment flows, and people movement into one policy storyline. The logic was straightforward: cut time and cost for trade, expand market access, and make cross-border movement more predictable.

Measure Value Meaning
Countries 151 countries Program reach
Combined GDP About $41 trillion Market scale
People covered ~5.1 billion Human scale

The chinese government framed the road initiative as a platform that uses state finance, SOEs, and diplomacy to deliver projects at scale. The ambition was clear, but formal policy blueprints were needed to convert vision into on-the-ground corridors.

From Vision To Implementation: The Policy Blueprint That Guided BRI Connectivity

The 2015 action plan framework translated a broad policy goal into a practical operating manual for cross-border work. It set out steps that made planning, finance, and people exchanges workable across many projects.

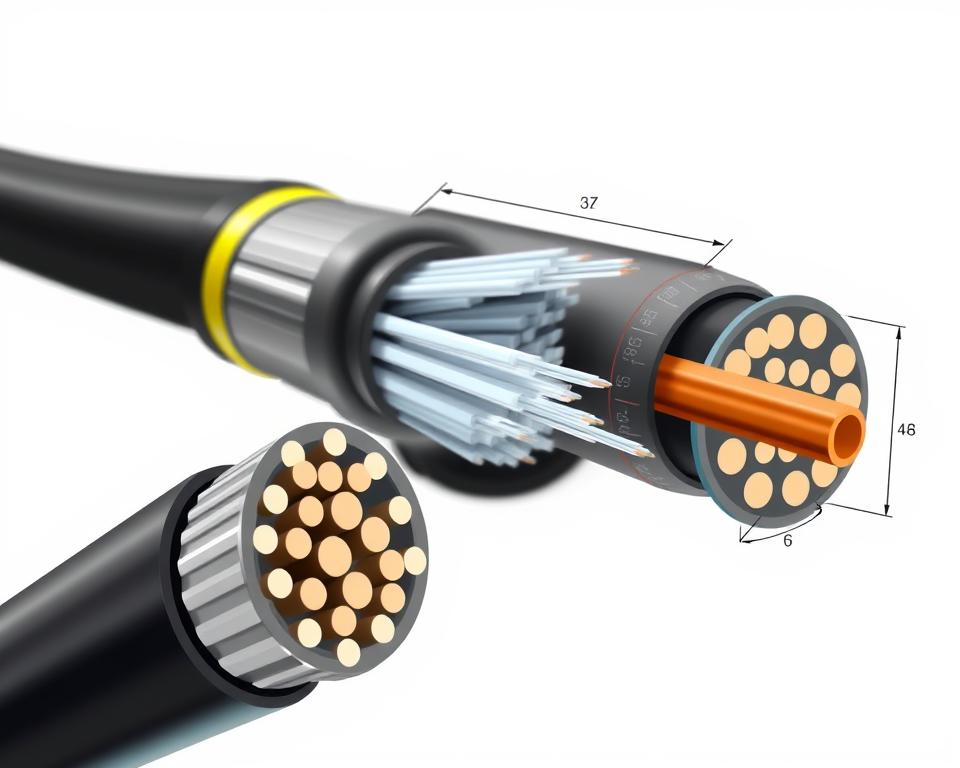
TTH Cable Production Line

The 2015 Action Plan Goals

The plan listed four targets: improve intergovernmental communication, align infrastructure plans, build soft infrastructure, and deepen people-to-people ties.

Government-To-Government Coordination

Stronger coordination meant national plans aligned at key stages. That reduced political risk and made projects less likely to stall after leadership changes.

Aligning Transport And Energy Systems

Plan alignment focused on connecting transport systems and power grids across borders. This approach aimed to supply industrial zones and urban growth with reliable routes and energy.

Soft Infrastructure And Financial Integration

Soft infrastructure included trade deals, harmonized standards, faster customs, and financial integration to ease cross-border payments and capital flows.

People-To-People Connections

Education exchanges, joint research, and tourism built the human networks needed to staff and sustain long-term projects.

Goal Area Primary Action Intended Result
Coordination Government forums Fewer policy reversals
Infrastructure alignment Transport and power mapping Connected routes, steady supply
Soft infrastructure Trade rules and finance links Smoother cross-border trade
People ties Scholarships & exchanges Local capacity plus trust

How The Silk Road Economic Belt And The 21st Century Maritime Silk Road Directed Routes

Two route systems—overland corridors across Eurasia and maritime networks at sea—set the spatial logic for major investments. This twin-track approach guided where capital, equipment, and construction teams concentrated over the past decade.
Financial Integration

Overland Links Across Eurasia And Central Asia

Overland corridors centered on rail, highways, and pipelines crossing Central Asia. Those corridors aimed to shorten transit times for exporters and cut reliance on long sea voyages.

Rail links through Central Asia became crucial as a bridge between producers and markets. Planners frequently integrated towns, terminals, and logistics parks into corridor plans.

Maritime Logistics: Ports, Sea Lanes & Hinterland Links

The Maritime Silk Road approach translated into three operational parts: port expansion, major sea-lane usage, and inland links that make ports functional. Ports served as hubs where ships meet rail and road for last-mile movement of goods.

Why Connecting Land And Sea Routes Mattered

Linking routes created strategic redundancy. When chokepoints threatened shipping lanes, overland options could divert traffic and keep goods moving.

Reliable route options increased predictability for shippers. That helps firms plan inventory, cut buffer stocks, and stabilize supply chains.

  • A two-route architecture concentrated capital on nodes that link land and sea.
  • Corridors converted route maps into bundled investments—ports, terminals, rails, and customs nodes.
  • On-the-ground projects needed financing, regulation, and operators working in concert.

Economic Corridors And Facilities Connectivity: What Corridor Development Meant In Practice

Building an economic corridor meant pairing hard works—roads, rail, ports—with softer measures that make places productive.

Corridor development was a package: transport links, logistics nodes, industrial clustering, and policy changes that ease trade. The goal was to turn transit routes into drivers of local growth.

Corridors As More Than Physical Infrastructure

Productive integration makes this plain. Manufacturing, power supply, and distribution networks were aligned so corridors created jobs and exports rather than just transit fees.

Planners added warehouses, customs hubs, and special zones to capture value close to the route. That helped move goods faster and supported local firms.

Where Corridor Planning Met Local Development

Local strategies—industrial parks, city-region plans, and land policy—aimed to capture spillovers from corridor projects.

Aspect Purpose Downside Case
Transport expansion Shorten travel time Underutilization if demand lags CPEC links multiple asset types
Industrial clusters Create jobs, exports Weak zoning blocks growth Special zones near terminals
Policy changes Faster customs, licensing Reform delays cut benefits Local alignment of trade rules

Over time, focus shifted from raw construction to utilization, revenue models, and long-run competitiveness. Corridor-scale work is capital-intensive and usually needs state-linked finance and strong political coordination to proceed.

Financing The Connectivity Push: Chinese Banks, Institutions & Competitive Bidding

Cheap, patient capital from Chinese policy banks rewired which projects could start and which stalled. That funding model was central to how many large transport and port projects progressed from 2013 to 2023.

Two policy lenders, China Development Bank (CDB) and the Export-Import Bank of China (EXIM), received large capital injections. Their bonds trade like government debt and they can tap People’s Bank liquidity. This gave them very low borrowing costs and flexible terms.

As a result, Chinese SOEs won many bids by offering attractive finance packages. From 2013 to 2023, roughly $1 trillion in investment and construction deals were signed with partner countries. That scale made cheap credit a defining characteristic of the initiative.

Competitive bidding often hinged on finance terms as much as technical offers. Recipient governments sometimes chose faster, lower-conditional loans over longer, conditional multilateral options.

Still, financing did not eliminate implementation risk. Indonesia’s high-speed rail offer won on strong Chinese investment and credit, but land acquisition and licensing delays slowed progress.

Beyond contracts, this model supported industrial policy: steady overseas pipelines kept SOEs busy and built execution experience. In turn, finance capacity shaped which sectors dominated early work—transport, energy, and port infrastructure—setting up the next phase of outcomes.

Past Project Patterns: Transportation, Energy & Ports That Anchored Facilities Connectivity

Early project patterns clustered around three physical pillars: transport routes, power buildouts, and major seaports. That mix made routes usable for trade and linked inland production to overseas markets.

Flagship Corridor Case: A Long Kashgar–Gwadar Link

The China-Pakistan Economic Corridor spans roughly 3,000 kilometers from Kashgar to Gwadar. The project bundles highways, rail, pipelines, and optical cables to give inland China faster maritime access.

Multi-Asset Bundles

Corridor bundles combined transportation nodes with power plants and digital links. Putting roads, rails, fiber, and grid works together shows how infrastructure went beyond single projects.
Belt and Road People-to-People Bond

Energy-First Investment Patterns

Many corridors prioritized energy. Large power plants and grid upgrades often came before industrial parks so factories would have reliable supply.

Ports And Strategic Nodes: Gwadar And Piraeus

Gwadar was leased to a Chinese ports operator until 2059, but rollout lagged—airport and free-zone timelines slipped and usable acreage remained small in 2023. That slowed cargo flows and local benefits.

By contrast, COSCO’s majority stake at Piraeus gave operators direct control and a foothold into European logistics. The two cases show how ownership structures and execution shaped real gains.

When energy, transport, and port work align, corridors cut costs and speed goods movement; when they don’t, utilization and benefits lag.

Economic And Trade Effects: How Connectivity Initiatives Influenced Growth And Integration

Shorter transit routes and smoother border processes made new markets reachable for many exporters. Reduced shipment time cut logistics costs and improved delivery predictability.

Companies could lower inventory buffers. That raised the appeal of exporting manufactured goods to farther markets and supported trade growth at regional scale.

How Moving Goods Faster Changed Trade

Lower transport costs and steady schedules increased traded volumes on several corridors. Faster delivery made perishable and time-sensitive products viable for export.

Measured effects included shorter lead times, cheaper freight per unit, and higher shipment frequency for some routes.

Financial Integration: RMB Use & Bond Issuance

Issuing RMB bonds and encouraging local currency use reduced currency friction. That helped buyers and lenders avoid costly currency conversions and built deeper capital links.

RMB-denominated instruments also made chinese investments easier to price and finance across borders.

Channel Mechanism Likely Effect Illustration
Transport improvements Shorter routes and better terminals Lower freight costs and faster delivery Rail and port packages
RMB bond issuance Local issuance and currency swaps Reduced exchange risk, deeper markets RMB bond programs
SOE capacity export Overcapacity deployed abroad Greater project supply, lower prices Steel and construction exports

Domestic Drivers And Regional Reshaping

Behind the projects were domestic aims: keeping state firms busy, exporting excess steel and cement, and deploying large national savings overseas.

Over time, expanding links can shift regional trade patterns and deepen some countries’ economic reliance on a major partner. That reshaping can raise productivity but also political leverage.

Partner countries may gain jobs, improved logistics, and growth if projects match local needs and governance is strong. However, benefits depend on sound project choice, transparency, and complementary reforms.

Scale creates both gain and risk. The same forces that raise trade and financial integration also amplify concerns about debt, governance, and underperforming projects—issues explored next.

Constraints And Controversies That Shaped Outcomes Over The Past Decade

A mix of financial strain, governance gaps, and execution bottlenecks shaped how many projects performed across partner countries. These limits drove policy shifts and changed how the public viewed large-scale investment programs.

Debt Stress And Warning Cases

Sri Lanka and Zambia became cautionary cases. Debt strain and repayment concerns shifted political debate and led some governments to renegotiate or halt deals.

“Repayment stress can reshape public opinion and force governments to rethink long-term commitments.”

Governance, Corruption Risks

Weak oversight increased value-for-money concerns. Low 2022 CPI scores—Turkmenistan (19), Pakistan (27), Sri Lanka (36)—help explain recurring concerns about transparency and fraud.

Execution Bottlenecks, Underperformance

Common delays came from land acquisition, licensing, procurement disputes, and cost overruns. Indonesia’s high-speed rail missed early targets for those reasons.

Kenya’s railway stopped short of the Uganda border, and a parliamentary review found rail freight could cost more than road transport. Incomplete networks lower returns and spark political backlash.

Limitation Example Effect Policy Action
Debt sustainability risk Sri Lanka, Zambia Renegotiation and public protests Loan-term review
Governance risks CPI low scores Value-for-money doubts Transparency initiatives
Execution delays Indonesia high-speed rail Cost overruns, slow use Tighter procurement rules
Underuse Kenya rail shortfall Reduced economic returns Project reappraisal

Geopolitics And The Pandemic-Era Slowdown

Geopolitical skepticism from the U.S. and some allies reduced high-level participation and pushed some countries away from large deals. Italy signaled shifting interest, for example.

Investment flows also dropped: outbound construction and investment in 2022 were $68.3B, down from $122.5B in 2018. That ~44% fall showed a clear momentum shift.

Taken together, these constraints pushed adaptation and set the stage for a 2023 pivot toward greener, digital, and integrity-focused cooperation.

How BRI Connectivity Began Evolving By 2023: From Megaprojects To Green And Digital Links

By 2023, the playbook had clearly shifted from headline megaprojects to targeted, lower-risk efforts. The white paper released in October framed the shift as a move toward smaller projects that emphasize sustainability, tech collaboration, and cross-border digital trade.

Signals From The 2023 White Paper And Forum Priorities

The 2023 white paper and the Third Forum emphasized a multidimensional network rather than one-off giants. Xi listed commitments that highlighted green development, science and technology cooperation, and stronger institutions.

New Emphasis: Green Development, Science & Technology, E-Commerce

Green development responds to environmental critiques and tighter financing. Smaller renewable projects and upgrade work can be approved and funded faster, with clearer permits and less social backlash.

Digital and e-commerce links widen the initiative’s scope. Data flows, platforms, and cross-border trade systems now sit alongside ports and rails as core parts of future integration.

Institution-Building And Integrity-Based Cooperation

A greater focus on integrity and institution building aims to manage debt and transparency risks. Stronger procurement rules, compliance checks, and joint oversight reduce political and financial friction for partners and lenders.

AI Governance And Shaping Rules

The Global Initiative for Artificial Intelligence Governance signals a move to set norms rather than only build assets. Rule-making in AI and standards work can shape influence across the 21st century as much as physical projects once did.

Implication: This pivot changes how partner countries measure success. Future influence will come from greener projects, digital platforms, and shared rules—tools that are harder to quantify but may prove more durable.

Conclusion

In summary: Years of rapid projects reshaped routes and reduced trade frictions, but outcomes differed by country. Success depended on solid economics, strong governance, and timely execution.

Over the decade the belt road approach moved from big, hard infrastructure builds to a more selective, reputation-aware agenda. By 2023 the initiative emphasized green work, digital links, and stronger institutions.

Core mechanisms to remember are route architecture (land and sea), corridor development logic, and financing driven by policy lenders and state firms. Major controversies—debt stress, corruption risks, execution delays, and geopolitical pushback—shaped the shift.

Watch next: green project pipelines, e-commerce platforms, and AI governance. For U.S. audiences, this evolution matters for standards, supply-chain routing, port influence, and the competitive landscape for development finance.

Related: Improving Adhesion in Fiber Secondary Coating Line Processes

From Sketch to Steel: The Designer’s Guide to CNC Precision Machining

At KZD-CncMmachining.com, you’ll find excels in delivering CNC Precision Machining expertise across many industries including aerospace, medical, energy, and automotive. It seamlessly blends advanced machining equipment alongside a team of experienced engineers. Their purpose is to transform intricate designs into tangible products. Leading facilities like RAM Tool and WessDel shops exemplify excellence with their expansive capabilities, commitment to ISO-certified quality systems, and a diverse array of machinery capable of managing substantial workpieces and demanding precision.

Precision CNC machining dramatically reduces production cycles, reduces waste, and improves product consistency. It’s accomplished by a synergy of CAD/CAM programming workflows, state-of-the-art machining centers, plus strict quality-control processes. A reliable CNC machine shop provides flexible CNC machining and contract manufacturing services. It proficiently adapts from initial prototype stages to comprehensive production volumes, with a focus on thorough inspection plus product traceability at every step.

At KZD-CncMmachining.com, we focus on a customer-centric approach, thorough metrological evaluation, plus providing complete start-to-finish solutions. Our experience serves both one-off CNC machining jobs and high-volume component production. Through an optimal combination of sophisticated machinery plus disciplined process control, we guarantee repeatable, accurate outcomes.

Main Takeaways

  • KZD-CncMmachining.com is dedicated to CNC Precision Machining for many industries.
  • High-end equipment including 5-axis machining and horizontal mills improves capability for complex parts.
  • Precision CNC machining reduces errors and increases repeatability through CAD/CAM and inspection.
  • Tailored CNC machining and scalable machining services support prototype to production runs.
  • Metrology and quality systems are vital to achieve strict tolerances and required industry standards.

CNC Precision Machining

Digital designs morph into precise parts across aerospace, medical, and industrial applications using CNC precision machining. Experts at facilities like RAM Tool and Precision Automation rely on CAD/CAM files for machine setup. They employ mills, lathes, and routers to create dies, prototype tooling, and specialized parts. Thorough inspections and punctual deliveries remain central to this workflow.

CNC Precision Machining

Definition And Core Benefits Of CNC Precision Machining Services

CNC production moves cutting tools through computer-based numerical control, ensuring exceptional accuracy. It significantly reduces manual setup, curtails cycle times, and limits errors. Services often include milling, turning, true 5-axis machining, and wire EDM, addressing complex shapes and demanding tolerances efficiently.

Typical Tolerances And Material Capabilities In CNC Machining

Precision CNC machining routinely reaches tolerances as minute as 0.0002 in. for steel and titanium alloys including Ti-6Al-4V alloy. Frequently machined stainless grades include 15-5, 17-4, 304, 316, and 420. The material mix extends from aluminum and zinc used in die casting to robust steels, titanium, and engineered plastics for a range of industrial needs.

How Precision CNC Machining Reduces Errors And Improves Repeatability

CAM programming, robust tool libraries, and automated probing curtail variation, improving consistency. Metrology tools, including CMMs and laser scanners strengthen part-to-part accuracy. This streamlines the move from prototypes to full production while ensuring rigorous quality control through traceable records.

Complete CNC Machining Services For Custom Parts

Manufacturers often need complete capabilities for rapid production of precision parts. Modern CNC machine shops marry milling and turning with specialized operations. This accommodates prototypes, limited runs, and extensive production volumes. Operations including RAM Tool, WessDel, and Precision Automation demonstrate integrated workflows. They improve design, inspection, and shipping processes for custom CNC machining projects.

CNC milling services address complex shapes and prototype fabrication utilizing multi-axis milling platforms and deep CAM libraries. Shops handle aluminum die-cast tooling projects and detailed features including pockets and ribs. Methods such as laser scanning and reverse engineering workflows strengthen inspection databases. This accelerates alterations and guarantees timelines are met.

CNC turning operations operations specialize in cylindrical parts and large-scale shaft production. Lathe-cell arrangements ensures uniformity and consistent quality finishes. Merging turning and live tooling enables complex parts to be produced in one sequence. This process cuts processing time and reduces costs for large production programs.

EDM and wire EDM techniques are solutions for complex designs in hard materials. These technologies craft narrow slots, sharp internal corners, and precise outlines unattainable by milling. Complementary procedures like heat treating, deburring, and finishing work ensure parts arrive ready for use.

Core Capability Typical Use Value Delivered
Multi-axis CNC milling operations Prototypes, complex contours, and die tooling Reduces setups, improves accuracy, and supports tight tolerances
CNC turning with live tooling capability Shaft production, bushings, threaded parts Speeds production, combines operations, cuts lead time
Wire EDM & EDM capability Hard materials, thin features, mold components Enables intricate shapes, maintains fine detail, preserves hardness
Laser scanning & metrology tools Reverse engineering, inspection, and quality control Confirms parts, supports revisions, ensures compliance
Heat treating & finishing Material strengthening, corrosion resistance, final appearance Delivers turnkey parts ready for assembly or end use

Selection of a proficient CNC machine shop involves matching equipment to part requirements. Look for facilities that combine milling, turning, and EDM with inspection and assembly capabilities. This synergy helps manage lead times. It ensures delivered parts match engineering intent.

Advanced Machining Technologies And Equipment In CNC Shops

Leading facilities deploy a coordinated mix, involving multi-axis platforms, swift centers, and formidable machinery for demanding designs and tight tolerances. The allegiance to esteemed brands, such as Hermle, DMG Mori, OKK, and Mitsubishi machines, underscores a devotion to enhanced productivity and consistency in precision machining.

5-Axis And Multi-Axis Machining For Complex Parts

Five-axis centers help engineers consolidate operations previously done across many setups. The application of genuine 5-axis machining speeds completion of parts with deep cavities, angled features, or complex shapes. This approach minimizes manual intervention, abbreviates the production cycle, while maintaining strict geometric fidelity, particularly for aerospace and medical devices.

High-Speed Machining Centers And Horizontal Boring Mills

High-speed milling adoption produces better surface finishes while shortening lead times for softer materials and composites. On the other hand, horizontal boring mills improve tool effectiveness while limiting problematic chip interference on large parts. Strategically combining high-speed and horizontal equipment enhances a shop’s versatility to adeptly tackle both small, detailed parts and large structures.

Coordinate Measuring Machines (CMM) And Metrology For Quality Assurance

A complete metrology approach integrates CMM probing, laser checks, and digital summaries for accurate comparison to CAD designs. Such sophisticated systems support strict AS9100 and ISO 9001 requirements. By linking measurement results to process adjustments, a top CNC facility reduces deviations while substantiating adherence to regulatory demands.

Integrating advanced machinery with a strong quality framework significantly reduces rejection rates and speeds the move to mass production. A smart mix of equipment and precision analysis provides scalable options, from prototypes through full-scale production.

Industry Applications And Material Expertise

Advanced CNC machining is essential for manufacturers to meet demanding requirements across industries. Companies such as RAM Tool, WessDel, and Precision Automation facilities highlight the importance of specialized processes and in-depth material knowledge to improve performance. They cater to industries including aerospace, medical, energy, automotive, mining, and heavy industrial equipment manufacturing.

Aerospace And Defense: Lightweight Alloys And Strict Standards

Components for aircraft and defense demand tight control over weight, strength, and fatigue resistance. Aluminum alloys and Ti-6Al-4V are frequently machined for airframes, engines, and structural parts. High-precision CNC machining adheres to tight tolerances while maintaining AS9100 traceability requirements.

Shops such as RAM Tool and WessDel produce parts that endure harsh conditions. They use processes including surface finishing and heat treatments, key for flight and defense applications. Their custom CNC machining work supports production of small flight hardware plus varied precision parts.

Medical And Life Sciences: Tight Tolerances And Traceability

Producing medical device components entails achieving micrometer-level tolerances while preserving rigorous traceability. Using clean-room practices and strong lot control is essential for meeting FDA and ISO 13485 requirements. Using precision CNC machining, these manufacturers can produce complex geometries for implants, surgical instruments, and diagnostic devices.

Material choices include stainless steels, cobalt-chrome, and titanium alloys. WessDel and similar specialized suppliers underscore the importance of documentation and serialization. This diligence ensures regulatory compliance and supply-chain integrity, enabling both prototype development and regulated production runs.

Energy, Automotive, Mining, And Industrial Equipment Applications

Across energy and heavy industry, durable parts made from hardened steels and specific alloys are essential. Machines such as horizontal boring mills is vital for machining large components. This CNC approach combines efficient material removal with heat control, producing consistent results.

Automotive and powersports manufacturers demand quick production times and consistent quality. By employing precision CNC machining, they cut waste and increase efficiency. Precision Automation, for instance, incorporates machining operations internally. This approach supports original equipment manufacturer assembly lines plus robotic subassemblies.

The table below offers a brief overview sector-specific needs, common materials used, plus machining priorities that shape supplier selection.

Industry Commonly Used Materials Key Machining Priorities
Aerospace & Defense Aluminum alloys, Ti-6Al-4V, nickel-based alloys Strict tolerances, traceability, surface finish, certification
Medical and Life Sciences Stainless steel (316L), cobalt-chrome, titanium Micron tolerances, lot control, clean-room processing
Energy and Power Hardened steels, Inconel, specialty alloys Large-format machining, heat-treat compatibility, wear resistance
Automotive and Powersports Steel, aluminum, case-hardened alloys High-volume repeatability, cycle-time optimization, cost control
Mining & Industrial Equipment Forged steels, wear-resistant alloys Durability, heavy-duty fabrication, large-capacity machining

Choosing suppliers with proven expertise in these materials reduces risk. Suppliers combining strong material expertise with verified CNC manufacturing deliver more predictable, cost-efficient paths from idea to production. That integration improves predictability and cost-efficiency for custom CNC machining projects.

Quality Systems, Tolerances, And Inspection Processes

Design intent transforms into reliable components through robust quality systems and stringent inspection protocols. CNC machining services combine ISO/industry standards with manual checks. This ensures compliance with aerospace, medical, and industrial specs. Production stays consistent, supported by clear traceability and thorough documentation from first run to full production.

Systems such as ISO 9001 and AS9100 provide ongoing control and audit readiness. WessDel operates within these standards, ensuring parts meet strict criteria. Precision Automation applies ISO 9001 practices together with CAD/CAM processes. This supports producing components that meet strict inspection requirements.

Inspection approaches vary by facility but use common tools: coordinate measuring machines (CMMs) for dimensional checks, laser scanning for complex shapes, and custom gauges to confirm fit and function. RAM Tool has a dedicated CMM inspection group, enhancing it with laser scanning for reverse engineering and superior quality assurance. These instruments are essential for confirming critical part characteristics.

A common inspection flow starts with CAD-driven tolerance review, followed by first-article inspection plus CMM verification. Laser scanning is employed to verify complex surfaces and assist reverse engineering. Complete documentation including serial numbers, approvals, and measurement data provides traceability.

Achievable tolerances depend on the selected material and machining method. In working with stainless steel and titanium, shops like RAM Tool can hold tolerances as tight as 0.0002 inch on select parts. Such precision underscores the importance of meticulous setups, dependable tooling, and skilled personnel within a focused CNC manufacturing environment.

Selecting a partner with precise metrology tools, defined procedures, and capable technicians is critical to achieve high-quality CNC machining outcomes. An efficient CNC machine shop incorporates thorough inspection processes into production, ensuring parts leave with confirmed compliance and reliable performance.

From Prototype To Production: Contract Manufacturing And Turnkey Solutions In CNC

Transitioning a concept into a tangible item entails a mix of prototype tooling skill, rapid changes, and substantial machining capacity. Companies like RAM Tool and WessDel illustrate the value of laser scanning and reverse engineering for faster prototype development. Precision Automation demonstrates integrated in-house machining plus assembly lines in delivering full-fledged systems, adhering strictly to ISO 9001 standards.

Prototype tooling & reverse engineering

Starting with fast fixtures and selective heat-treat or surface-finish improvements, prototype tooling sets the foundation. Using laser scanning, teams capture existing-part dimensions for reverse engineering, helping bypass extensive CAD redraws. This method greatly reduces the iteration phase, supporting an optimized fit while maintaining high-quality parts.

Scalable contract manufacturing

Contract manufacturing extends from low-volume lots for validation to high-volume production for launch. At every stage, custom CNC machining transitions from single-item operations to automated cell layouts. When production scales up, CNC machining services adeptly adjust programming, tooling setups, and inspection processes.

Subassembly, wiring & machine rebuilding

Turnkey solutions often include subassembly, automated wiring of control panels, and comprehensive machine renovations. Subassembly services reduce customer assembly workload. Renovating and updating machines extends service life and helps conserve capital for manufacturers, ensuring reliable production uptime.

Capability Common Offerings Value to Customers
Prototype tooling Rapid fixtures, soft jigs, small-batch molds Speedier validation, lower upfront costs
Reverse Engineering Services Laser scanning, CAD recreation, fit checks Recreate legacy components, cut redesign time
Custom CNC Machining Services 5-axis milling, turning, precision finishes Accurate, repeatable production
Contract Manufacturing Services Low- to high-volume runs, kitting, logistics Scale without capital expansion
Subassembly & Wiring Services Automated panel wiring, functional tests Plug-and-play delivery, reduced assembly time
Machine Rebuilding Services Refurbish spindles, retrofit controls Extended asset life, improved performance

Opting for a collaborative partner with vast capabilities in CNC manufacturing minimizes transitions and expedites timelines. Embedding design-for-manufacture insights and comprehensive CNC machining services into a unified contract manufacturing arrangement ensures clarity of responsibility. This facilitates faster time-to-market for new products.

Choosing A CNC Machine Shop: What To Look For In A Partner

Choosing the right partner for precision work is essential. A leading CNC machine shop pairs strong technical skill, modern equipment, and dependable service. Look for a shop with proven quality systems, clear capacity and capability visibility, plus demonstrable experience in your sector.

Technical Expertise, Experienced Machinists, And Engineering Support

Make sure the shop staffs competent machinists proficient in CAD/CAM software, backed by engineering support. Working together on design improves manufacturability, reduces errors, and speeds project completion. Inquire about their experience with intricate CNC machined parts and request references from analogous endeavors.

Facility Scale, Machine Brands, And Capacity

Review the shop’s floor space, its lifting and heavy-load capacity, and the diversity of its machinery. Large facilities with advanced 5-axis centers, multiple CNC stations, and strong lifting equipment can handle large, complex projects. Select facilities demonstrating commitment to excellence by using reputable machine brands such as Hermle, DMG Mori, OKK, and Mitsubishi machines, which ensure unwavering precision in CNC machining operations.

Customer Service, On-Time Delivery, And Industry-Specific Experience Factors

Seek establishments with ISO/AS9100 certification for jobs requiring meticulous traceability. Shops with a track record of on-time delivery and offer comprehensive CNC machining solutions reduce operational complexity, cutting transition time and oversight. Pick a partner providing in-house inspection, CMM checks, and secondary processes to support efficient quality management.

Checklist:

  • Verified quality systems (ISO, AS9100)
  • Machine list with 5-axis and horizontal capabilities
  • Evidence of precision CNC machining plus CNC services
  • References from your industry and on-time delivery stats
  • In-house inspection, assembly, and turnkey capability

Final Thoughts

Top-tier shops meld broad capacity, capable teams, and modern equipment to deliver reliable CNC Precision Machining across industries. From CAD/CAM-driven prototypes to volume production, their precision machining minimizes errors and accelerates market readiness. A capable CNC shop combines milling, turning, and EDM. It performs strict inspection to satisfy demanding standards across aerospace, medical, and energy industries.

Adherence to ISO 9001 and AS9100 standards, along with expertise in 5-axis machining and metrology shows a partner can manage tight tolerances and traceability needs. Custom CNC machining improves when engineers and machinists collaborate early to refine designs for manufacturability, ensuring consistent quality. Integration services provided by turnkey specialists, along with in-house CNC manufacturing capabilities abbreviate lead times and mitigate risks by centralizing operations.

For U.S. enterprises in pursuit of reliable output, partner selection should be based on measurable inspection capability, documented procedures, and a proven record producing complex components. The best CNC machine shop balances technology, people, and process excellence. This harmony creates a foundation for effective CNC Precision Machining and long-term supply reliability.

Related: Turning And Milling CNC Precision Parts

Supply Chain Resilience Through AMT CIM Manufacturing Partnerships

Understanding Ceramic Injection Molding for High-Precision Components

Is it possible for one manufacturing route to provide metal-like tolerances, complex shapes, and heat-resistant materials in a single process?

This is a concise guide to a scalable manufacturing technology that enables complex, high-precision ceramic parts — https://amt-mat.com/business/mim/ceramic-injection-molding/. In this method, fine powder is mixed with a binder to produce a moldable feedstock. That feedstock is then shaped by injection, debound, and sintered to near-theoretical density.

Its major benefits are broad design freedom, repeatable output, tight dimensional tolerances, and surface quality on par with many metal processes. It fits especially well when CNC or tape casting struggle with small, intricate parts.

Because sintering introduces shrinkage, anticipating dimensional change in the design phase helps minimize rework and expense. This manufacturing route supports mid-to-high production volumes where tooling cost and cycle time are justified by part counts.

Use cases include aerospace, automotive, medical, electronic, and industrial parts that must resist wear, high temperature, or corrosive conditions. In this article, we move from materials selection through QA, highlighting how simulation and metrology tools support consistent, reliable parts.

ceramic injection molding

What Is Ceramic Injection Molding and Why It Matters Today

The injection molding route for fine-powder parts uses a thermoplastic or wax binder mixed with powder to form a flowable feedstock. The feedstock then fills complex mold cavities, forming green parts with features that are difficult to achieve with slip casting, dry pressing, or isostatic pressing.

How it differs from traditional methods

Unlike slurry or powder compaction methods, this route supports internal channels, undercuts, and thin walls in small-to-medium components. Production throughput is generally higher, with reduced variability compared to many manual processes.

Where It Fits into Modern Manufacturing Workflows

A typical process flow is: design for shrinkage → build tooling → perform molding → carry out debinding → run sintering → apply finishing. Cycle times often range from seconds to a few minutes per shot. Ideal volume ranges are mid-to-high runs where tooling investment is recovered.

“Using DOE trials and pilot runs for design validation cuts risk before full production.”

Forming Method Geometric Capability Output Rate Labor
Feedstock-based route High — supports undercuts and internal channels High throughput Low, highly automatable
Traditional slip casting Moderate Low throughput High
Isostatic and dry pressing From simple to moderately complex Moderate Medium labor need

After sintering, lapping or laser-based features can be applied to refine tolerances. The route aligns well with SPC and PPAP systems, improving traceability and process control. The clear advantages today are efficiency, lower scrap, and the ability to unlock designs otherwise too costly.

Fundamental Principles of Ceramic Injection Molding

This section explains the step-by-step route that converts fine powder and binder into a dimensionally stable part prepared for sintering.

Turning Powder and Binder into a Finished Component

Start by selecting powder with the right particle size distribution and surface area. These characteristics govern packing density, feedstock viscosity, and the eventual microstructure.

  • Combine the powder with a customized binder system and compound it into feedstock with a solids loading usually around 55–65 vol%.
  • Use injection to form a green part; pay attention to gate placement to avoid weld lines and uneven packing.
  • Debind to produce a fragile brown part, then sinter to near-theoretical density.

Binders need to flow well to fill the mold, support shape during handling, and be removed cleanly in debinding to prevent blisters and cracks.

Feedstock rheology, specifically viscosity as a function of temperature and shear, controls fill behavior, knit lines, and surface quality. CIM machine design, including screw and barrel geometry, helps maintain feedstock homogeneity and limits degradation.

“Control the processing window: small deviations in temperature or pressure often cause short shots, voids, or poor surface quality.”

Relative to MIM, ceramic injection molding uses higher sintering temperatures and modified atmospheres to align with ceramic chemistries and densification requirements.

Materials and Feedstock Preparation for High Precision Ceramic Parts

The choice of powders and binders establishes the base for consistent, high-precision components.

Choosing Powders and Key Specifications

Alumina excels where wear resistance and electrical insulation matter for AMT. Zirconia provides improved fracture toughness in components that experience shocks. Silicon carbide is suitable for high-temperature, highly abrasive environments.

Carefully control particle size, morphology, and purity. Using fine, spherical powder tends to improve packing and the resulting surface quality. Irregular-shaped particles can increase green strength yet may lead to a rougher final surface.

Binder Systems and Their Ratios

Typical binder families include waxes and polyolefins like polyethylene and polypropylene, supplemented by specialty polymers for challenging geometries. Binder percent affects melt flow and debinding time.

Compounding and rheology

Use a steady compounding sequence: dry-blend the powder, add polymer gradually, then apply controlled temperature and shear. Keep peak processing temperatures in check to avoid degrading the binder system.

Use capillary or torque rheometry to verify that the viscosity window supports reliable filling and packing. Aim for solids loading that balances density and shrinkage — typically around 55–65 vol% for high-density parts.

Storage, Handling, and Drying Practices

Store powders in sealed containers and use FIFO. Control humidity for hygroscopic additives, and dry pellets prior to molding to cut down on voids and blemishes.

Follow PPE and dust controls when handling fine powder and hot polymers. Early supplier collaboration on powder and binder choices speeds validation and lowers iteration risk.

How to Design Parts Specifically for Injection Molding

For this process, design efforts start with clear goals: hitting tolerances and reducing post-sinter operations. Early CAD decisions govern shrinkage behavior, mechanical strength, and handling of fragile green parts.

Wall thickness, gates, and knit line management

Aim for uniform wall thickness with smooth transitions to reduce sink and warping. Place gates so that flow moves away from cosmetic or high-stress regions, limiting knit lines in those areas.

Create a shrink map and scale mold features so final dimensions fall within the required range. Validate with flow simulation and a DFM review before tooling.

Draft, radii, and features for debinding/sintering

Provide modest draft angles and generous radii to ease demold and lower stress concentrations. Integrate vents, sacrificial channels, or setters to speed debinding and support fragile shapes.

Define datums and inspection features based on how parts are fixtured during sintering and quality checks. Provide just enough finishing stock for critical fits, preventing unnecessary extra material and cost.

Design Area Key Recommendation Outcome Verification
Wall thickness Uniform, gradual transitions Reduced warpage and more predictable shrinkage Simulation or prototype trials
Gate Location Keep out of cosmetic and high-stress zones Lower incidence of knit-line defects Mold flow analysis
Debinding features Add vents, channels, and setters Safer brown parts; fewer cracks DFM and process review

Tooling and Mold Considerations for Ceramic Injection

Good tooling design reduces scrap levels and strengthens dimensional consistency across extended production. Start by choosing tool materials and surface treatments that withstand abrasive feedstock and tight tolerances.

Tooling materials must withstand abrasion and repeated thermal cycling. Use high-grade steels or nickel-based alloys with wear-resistant coatings to prolong tool life.

Balance surface finish to aid release while preserving detail. Steer clear of click here textures that capture binder and encourage sticking. Design vents to remove air and volatiles effectively, reducing burn marks and incomplete fills.

  • Choose gate types (edge, submarine, hot tip) and runner layouts to promote balanced filling and reduce weld lines.
  • Refine cooling circuits to hold cavity temperatures steady and reduce variation between cycles.
  • Use robust ejection systems, such as stripper plates or air assist, to protect fragile green parts during demolding.
  • Fit interchangeable inserts for quick iteration on gates, vents, and critical dimensions.
  • Account for tolerance stack-ups by adjusting cavity dimensions for expected shrinkage.
  • Integrate in-cavity sensors for pressure and temperature to track the process and support closed-loop control.
  • Schedule maintenance intervals and abrasion inspections to keep performance consistent over long runs.

These measures tighten dimensional control and reduce downstream rework. They also support scalable production using modern molding technology while protecting tool investment.

Step-by-Step Guide to Running the Injection Molding Stage

A repeatable press cycle relies on stable temperature profiles, controlled pressure ramps, and consistent operator discipline. Start with a clear start-up checklist that safeguards both feedstock and machinery from thermal shock.

Machine Setup: Temperature, Pressure, and Injection Speed

Set barrel and mold temperature profiles to keep viscosity stable without degrading the binder. Tune injection speed and pressure profiles so complex features fill fully without jetting or visible flow lines.

Filling, Packing, and Cooling for Tight Tolerances

Use multi-stage packing to densify green parts and reduce internal voids. Balance cooling time for handling strength and cycle efficiency. Implement purging and material changeover steps to avoid cross-contamination.

Demolding without damaging green parts

Apply low-friction coatings and measured mold release where needed. Rely on gentle ejection and protective fixtures to support delicate green features. Train operators to recognize defects early and halt production if necessary.

Key Control Primary Target Key Benefit
Barrel and mold temperature Stable viscosity behavior Fewer short shots; consistent surface
Pressure and speed ramps Programmed multi-stage profile Complete fill; reduced weld lines
Packing & cooling Balanced multi-stage strategy Stable density and controlled dimensions

Debinding Methods and Best Practices

Effective binder removal is a critical step that converts a fragile green part into a sinter-ready component.

In practice, two debinding methods dominate: solvent-based debinding and thermal debinding. Solvent debinding extracts the soluble binder fraction first. Subsequent thermal debinding eliminates the remaining polymer through controlled pyrolysis.

Solvent Versus Thermal Debinding Approaches

Solvent debinding quickly removes soluble phases and lowers internal pressure during subsequent stages. Thermal debinding is slower but needed to remove hard-to-dissolve polymer. Selection of the method is driven by binder formulation and part shape.

How to Avoid Debinding Defects

Fixture selection and part orientation are important. Support fragile areas and allow free escape paths for volatiles to prevent cracking and distortion.

Use gentle heating ramps, staged hold times, and controlled airflow to avoid pressure spikes that cause blistering. Thick sections and blind holes need longer cycles or local vents.

Choose recoverable solvents and maintain effective ventilation. Follow MSDS guidance along with local environmental regulations to safeguard workers and maintain compliance.

  • Use test coupons and sacrificial parts to confirm full binder removal prior to sintering.
  • Look for odd odors, color changes, or irregular mass-loss profiles as signs of incomplete debinding.
  • Troubleshoot skin formation, delamination, or slump by slowing ramps, improving venting, or adjusting fixture layout.

Debinding outcomes are strongly influenced by molding quality—voids or knit lines can become failure sites in this stage. Record debinding curves and mass loss data to standardize processing and protect final part quality.

Sintering for Final Density and Performance

Carefully controlled sintering is the step that converts a fragile brown shape into a dense, service-ready part. Furnace recipes establish microstructure, porosity, and mechanical behavior that dictate long-term performance.

Temperature profiles, atmospheres, and shrinkage control

Use a three-stage profile: slow heat-up to remove residual binder, a controlled ramp into the densification range, and a measured cool-down to avoid thermal shock.

Select an atmosphere appropriate to the material: air for oxide ceramics like alumina, inert or reducing atmospheres for carbides and certain engineered mixes. The right gas preserves chemistry and color while limiting grain boundary reactions.

Measure shrinkage with sacrificial coupons and incorporate those values into cavity compensation. Design setters and supports to restrain warpage and allow uniform gas flow.

Achieving Strength, Corrosion Resistance, and Wear Resistance

Sintering adjusts grain size and porosity, which in turn drive flexural strength and fracture toughness. Aim for high density with minimal grain coarsening to meet mechanical targets.

Tune material chemistry and soak schedules to maximize corrosion resistance and surface hardness for wear. Use post-sinter HIP when remaining porosity compromises fatigue or sealing behavior.

  • Record sintering recipes and verify furnace behavior using thermocouples or suitable pyrometry.
  • Control part orientation and spacing to ensure even temperature and atmosphere exposure.
  • Watch for defects such as slumping, excessive grain growth, and trapped porosity; gentler ramps and better support often correct them.
Parameter Recommended Target Impact on Part Properties Practical Tip
Ramp Rate 1–5 °C/min (debinding) / 5–20 °C/min (sinter) Reduces cracking; controls grain growth Match ramp to binder chemistry and part mass
Soak Temperature and Time Material-specific peak; minutes–hours Increases density and closes porosity Use test coupons to fine-tune soak
Gas atmosphere Air, inert, or reducing, depending on material Preserves chemistry; prevents oxidation Monitor gas flow and purity continuously
Post-sinter options HIP and/or anneal Reduces porosity and enhances mechanical strength Use for parts that require maximum performance margins

“Stable sintering recipes and validated furnace performance directly improve yield and reduce finishing rework.”

Quality Control, Metrology, and Tolerances

With a solid metrology plan, shrinkage uncertainty can be turned into reliable tolerance control. Set inspection gates at the green, brown, and sintered stages so variation is caught early.

Shrinkage Measurement and Mold Compensation

Use shrinkage correlation charts generated from pilot runs to scale cavity dimensions. Confirm results using sacrificial coupons, then update the mold compensation map prior to full production.

Surface Quality, Microstructure, and Porosity Checks

Use profilometers and Archimedes-based density checks to examine surface finish and density. Micro-CT and optical scans reveal internal pores that affect mechanical properties.

  • Set inspection plans for green, brown, and sintered parts with explicit pass/fail gates.
  • Use CMMs, optical scanners, surface profilometers, and micro-CT to verify both external and internal features.
  • Correlate grain size and pore distribution with strength and wear performance.
Stage Measurement Tool Metric Follow-up Action
Green parts Optical scanning Dimensional match to design Adjust mold compensation factors
Brown stage Micro-CT Void and pore distribution Modify the debinding cycle
Sintered parts CMM and surface profilometer Final dimensions and surface roughness (Ra) Lock process and release for production
Lot-level control Statistical process control tools Cp, Cpk, density Hold or release lots

Implement SPC and capability studies prior to PPAP. Maintain traceability from powder and binder lots through each production batch. Ensure gauges are calibrated, run MSA, and set nonconformance workflows with defined root-cause and corrective actions.

“Reliable measurement and traceable data close the loop on production quality.”

Applications and Use Cases in the United States

Domestic producers prefer feedstock-based production for parts that must combine low mass with high wear resistance. In aerospace, automotive, medical, and electronics industries, this route serves suppliers needing tight specifications and robust environmental performance.

Aerospace: High Strength-to-Weight Components

For aerospace, manufacturers often select lightweight wear components, nozzle inserts, and thermal barrier parts that require high strength-to-weight performance.

These components help improve fuel efficiency and withstand temperature cycling and vibration in engines and actuation systems.

Automotive: Thermal Stability and Durability

Automotive applications cover pump elements, sensor housings, and exhaust-related insulators requiring thermal stability and long-term durability.

Shifting from metal to engineered powder components helps reduce corrosion and lengthen service life under demanding under-hood conditions.

Medical and electronics: miniaturization and precision

Medical and electronics markets benefit from micro-scale insulators, ferrules, implantable device components, and biocompatible wear parts.

These components demand tight tolerances, high dielectric performance, and validated biocompatibility or dielectric testing before production release.

  • Performance-related edge: superior wear resistance and corrosion resistance make these parts ideal for harsh service.
  • Many regulated manufacturers operate under AS9100, IATF 16949, or ISO 13485, with extensive documentation and traceability.
  • Design-for-assembly is important for hybrid systems that join these parts to metals or polymers.
Stage Typical U.S. Lead Time Remarks
From tooling to pilot Roughly 6–12 weeks Depends on insert complexity
From pilot to SOP Typically 4–8 weeks Covers validation and qualification testing
Total Timeline Roughly 10–20 weeks total Domestic supply chains help shorten logistics and lead times

Validation steps include biocompatibility studies for implantable components and dielectric testing for electronic parts. Many case studies show this route replacing metal designs, reducing weight and eliminating corrosion-related failure modes.

Costs, Cycle Times, and When Ceramic Injection Molding Beats Machining

Grasping the economic picture helps you decide if formed-powder production or traditional machining is the smarter choice. Start by identifying core cost drivers and understanding how cycle time influences cash flow.

Key cost drivers

Tooling and mold amortization often dominate initial spend. High-performance steels and interchangeable inserts bump up initial expense but shrink per-part cost at higher volumes.

Material/feedstock usage, press time, furnace soak duration, labor, and yield losses all contribute to true landed cost. Secondary finishing, inspection, and packaging also play a notable role.

Cost Driver Impact How to reduce
Tooling / mold High up-front; lowers per-part at scale Use modular inserts and spread cost over more units
Feedstock and material Recurring; strongly influences density and scrap rates Negotiate lots; optimize solids loading
Machine and Furnace Time Sets throughput and cash flow Balance press cycle with sinter batch size
Yield/Rework Hidden cost driver Design for uniform walls and gate locations

When it beats machining

For complex geometries and mid-to-high volumes, per-part costs typically fall below machining costs. Working brittle blanks by machining can generate high scrap and lengthy cycles for internal features.

Traditional machining still prevails for very small runs, large parts, or where very tight post-sinter finishing is necessary.

“Optimized designs and well-planned batches are what transform fixed costs into attractive per-part pricing.”

Useful Heuristics for Quoting

  • Estimate tooling payback by dividing tooling cost by expected units to get a per-part tooling cost.
  • Add material, machine time, furnace time pro rata, labor, QA, and packaging to obtain unit cost.
  • Build in a scrap buffer of about 5–15% and allocate budget for secondary finishing.

These steps frame total cost of ownership and show where design, process choices, and smarter tooling deliver the biggest advantages.

Troubleshooting Common Ceramic Injection Molding Defects

Identifying the root cause of short shots or warpage calls for reliable data and systematic troubleshooting. Use a simple checklist to separate issues originating in molding, debinding, or sintering.

Common Defects and How to Diagnose Them Quickly

Short shots and voids occur when injection speed or pressure is too low, vents are blocked, or the feedstock contains excess moisture.

Warpage is often caused by uneven packing, nonuniform cooling, or insufficient support during sintering.

Weak knit lines and delamination usually respond to improved gate design, elevated melt temperatures, or better flow balancing among cavities.

  • Debinding blistering or cracking: typically due to ramp rates that are too fast, uneven part mass, or poor solvent penetration.
  • Inspect for mold wear or cavity damage when new defects emerge late in a production campaign.
  • Use incoming inspection to monitor feedstock variability and moisture content.

“Structured tools like Ishikawa diagrams and the 5-Whys help isolate which stage is driving failures.”

Defect Likely Cause Fast Action
Short shot/void Insufficient pressure/speed or blocked vents Increase injection pressure; clear vents
Warpage Uneven packing/cooling Balance cavity filling and adjust cooling
Blistering/cracking Debinding ramp or solvent issue Slow down ramps; evaluate solvent system

Use DOE studies to optimize parameters and validate corrections. Track defect codes and use Pareto charts to focus continuous improvement. Create tight feedback loops between press operators, furnace staff, and QA to speed corrections and improve overall quality.

Safety, Regulatory Compliance, and Sustainable Processing

Protecting workers and the environment is just as important as meeting tolerances in modern powder-based production.

Handling powders and binders safely

Use PPE: N95 or P100 respirators, chemical-resistant gloves, eye protection, and protective clothing for dry powder and hot binder work.

Install local exhaust ventilation and HEPA filtration to control fugitive dust. Enclose transfer points and ensure transfer lines are grounded to mitigate static hazards.

“Train staff on spill response, binder hazards, and safe storage—regular drills simplify audits.”

Managing Waste, Recycling, and Energy Use

Separate waste into distinct streams—powder, used binder, solvent residues, and general trash. Label containers and keep solvent and powder streams separate for recovery.

Use closed-loop solvent recovery and carefully controlled regrind of feedstock where quality is maintained. This reduces disposal costs and preserves raw materials.

Schedule furnace loads to maximize fill rates and minimize peak energy demand. Upgrade insulation, use high-efficiency motors and variable-speed drives, and log energy data to support ISO 14001-style continuous improvement.

Follow OSHA and EPA rules for hazardous air pollutants, solvent emissions, and recordkeeping. Ensure procedures, training logs, and MSDS documents are maintained and available for audits.

Design parts to cut mass and cycle time—these simple choices lower energy use and offer clear environmental advantages while keeping production reliable.

Next Steps: Moving Your Ceramic Injection Molding Project into Production

Turn design intent into reliable production by sequencing material trials, tool proofs, and pilot runs.

A practical checklist: select feedstock, conduct a DFM review, simulate flow, build a prototype mold, run validation builds, then perform PPAP or its equivalent.

Set milestones from RFQ → prototype tool → capability studies → first article inspection → SOP. Agree on deliverables and timelines with suppliers to reduce risk in early decisions.

Document control plans, work instructions, and key quality metrics before beginning pilot production. Plan capacity to cover press tonnage, furnace size, debinding throughput, and available staffing.

Focus on early successes using parts that benefit most from precision and complex geometries. Maintain quality with preventive maintenance, gauge R&R, and periodic requalification.

Ready to proceed? Ask for a feasibility assessment and cost model aligned with your parts, volume expectations, and performance targets.

FAQ

What is the process behind making precision ceramic parts with injection techniques?

The process starts by mixing fine oxide or carbide powder with a polymer-based binder to form a homogenous feedstock. That feedstock is shot into a mold under pressure to create a green part. After molding, the binder is removed through solvent or thermal debinding, and the part is sintered to reach final density and mechanical properties. Every stage — compounding, molding, debinding, and sintering — must be carefully controlled to meet tight tolerances and performance goals.

How is this approach different from traditional pressing or slip casting?

Unlike pressing or slip casting, which often shape parts individually and may require considerable machining, injection supports high-volume production with complex geometries, fine features, and high repeatability. This method frequently cuts down post-sinter machining, raising material yield and reducing per-part cost as volume increases.

Which powders are most commonly chosen for high-precision CIM parts?

Frequently used powders are alumina, zirconia, and silicon carbide. Tungsten carbide blends appear where extreme wear resistance matters. Powder selection depends on required strength, thermal stability, corrosion resistance, and electrical properties. Powder surface chemistry and particle size distribution also influence feedstock flow and the final achieved density.

How do binders function in the process and how are they chosen?

Binders provide cohesion and flow during molding, then must be removable without harming the part. Binder systems usually combine waxes and polymers in controlled ratios to achieve viscosity, green strength, and predictable debinding. Selection depends on part geometry, debinding method, and environmental or safety requirements.

How are shrinkage and tight tolerances handled in design?

Designers compensate for predictable sintering shrinkage by scaling mold cavity dimensions. They also control wall thicknesses, add radii, and locate gates to minimize knit lines and deformation. Close collaboration with manufacturers helps define realistic tolerances based on material and process capability.

What mold considerations affect part quality?

Filling, packing, and demolding behavior is shaped by mold material, surface finish, vent design, and gate/runner layout. Hardened steels with polished cavities reduce surface defects. Proper venting prevents trapped gas and short shots, while optimized gates yield consistent feedstock flow and reduce weld lines.

What is done during molding to achieve tight dimensional control?

Machine parameters such as barrel/mold temperature, injection speed, and holding pressure are tuned to secure full cavity fill and consistent packing. Cooling/demolding timelines are tuned to prevent green-part distortion while preserving good cycle times. Monitoring process data helps keep variation low.

Which debinding methods are used and in which situations?

Solvent debinding removes soluble binder fractions and is relatively gentle on complex geometries. Thermal debinding uses controlled heating to evaporate or pyrolyze residual binder, frequently following solvent debinding. The choice depends on binder chemistry, part thickness, and risk of cracking or blistering.

How are cracking or blistering defects avoided during debinding?

They control heating rates, ensure venting paths, and use staged solvent/thermal sequences tailored to feedstock. Uniform binder removal and minimizing internal pressure during decomposition reduce stresses that cause cracks or blisters.

What sintering practices ensure final strength and wear or corrosion resistance?

Sintering profiles — temperature, hold time, ramp rates, and atmosphere — are optimized for densification while limiting grain growth. Controlled atmospheres or isostatic post-sinter densification may be used to achieve target density, strength, and surface properties like wear and corrosion resistance.

How is consistent quality maintained from run to run?

Quality control relies on dimensional inspection (with shrinkage compensation), microstructure review, porosity checks, and mechanical testing. Statistical process control is applied to key parameters, and first-article inspection confirms that tooling compensation and sintering produce the desired results.

Which U.S. industries benefit most from ceramic injection molding?

The largest benefits are seen in aerospace, automotive, medical device, and electronics industries. Common applications are thermal/wear-resistant parts, high-strength tight-geometry components, and miniature parts that are difficult or expensive to machine.

When does this approach beat traditional machining on cost?

It becomes cost-effective when volumes are moderate to high, geometries are complex, or part consolidation eliminates assembly operations. High tooling costs are amortized over many units, and reduced machining cuts material waste and cycle cost per component.

Which common molding defects should teams monitor and how can they be diagnosed?

Short shots, voids, warpage, and delamination typically arise from feedstock variability, inadequate mold venting, incorrect machine settings, or improper debinding/sintering conditions. Root-cause analysis maps defect location to process step, then isolates variables like pressure, temperature, or feedstock rheology for correction.

Which safety and environmental issues matter most with powders and binders?

Use local exhaust ventilation, dust-control systems, and proper PPE when handling fine powders. Handle solvent and binder waste in line with OSHA and EPA rules. Recycling of scrap feedstock and energy-efficient sintering reduce environmental footprint.

How should a company start when moving a prototype into production?

Begin with material selection and a design-for-manufacturability review. Make pilot parts to confirm feedstock performance, mold compensation, and furnace settings. Refine tooling and process parameters iteratively and partner with qualified suppliers capable of consistent metrology and controlled processes.

Turning And Milling CNC Precision Parts

CNC Precision Machined Parts: Precision Engineering Services

About 70% of today’s critical assemblies depend on narrow tolerances to achieve safety and functional targets, a reminder of how small variances affect outcomes.

High-accuracy CNC titanium manufacturing improves overall reliability and operational life across auto, healthcare, aviation, and electronics applications. It provides repeatable mating, faster assembly, and fewer do-overs for downstream teams.

Here we introduce UYEE-Rapidprototype.com as a vendor dedicated to satisfying rigorous requirements for regulated industries. Their approach blends CAD with CAM, proven programming, and controlled systems to control variability and accelerate launch.

This guide enables US purchasers weigh choices, define explicit requirements, and choose capabilities that match applications, budgets, and timelines. Use this practical roadmap covering specs and tolerances, equipment and processes, materials and finishing, industry use cases, and pricing drivers.

CNC titanium machining

  • Precision and repeatability enhance reliability and decrease defects.
  • Digital workflows like CAD/CAM support repeatable manufacturing performance.
  • UYEE-Rapidprototype.com is positioned as a capable partner for US buyers.
  • Explicit, measurable requirements help match capabilities to project budgets and timelines.
  • Appropriate processes reduce waste, accelerate assembly, and reduce TCO.

CNC Precision Machined Parts: Buyer’s Overview for the US

US manufacturers need suppliers that deliver reliable accuracy, lot-to-lot repeatability, and predictable lead times. Teams need clear schedules and parts that pass acceptance so downstream assembly/testing remains on schedule.

Current buyer priorities: accuracy, repeatability, lead time

Top priorities are tight tolerances, consistent batch-to-batch repeatability, and stable lead times even as demand shifts. Robust quality systems and a disciplined system reduce variance and increase confidence in downstream assembly.

  • Accuracy aligned to drawing/function.
  • Lot-to-lot repeatability for lower QA risk.
  • Predictable lead times and open communication.

UYEE-Rapidprototype.com’s support for precision projects

They provide timely quotes, design-for-manufacture feedback, and buyer-aligned scheduling. Processes employ validated machining services and robust programming to minimize schedule slips and rework.

Lights-out, bar-feed production enable scalable production with reduced cycle time and stable precision when volumes increase. Early alignment on prints and sampling keeps QA/FAI on time.

Capability Buyer Benefit When to Specify
Validated machining services Lower defect rates, predictable yield Regulated/high-risk programs
Lights-out automation Faster cycles, stable accuracy Large or variable volume production
Responsive quoting & scheduling Quicker launch, fewer schedule surprises Rapid prototypes, tight schedules

Selection Criteria & Key Specifications for CNC Precision Machined Parts

Clear, measurable selection criteria turn drawings into reliable production outcomes.

Benchmarks: tolerances, finish, repeatability

Define precision machining tolerance targets on critical features. As tight as ±0.001 in (±0.025 mm) are attainable when machine capability, fixturing, and temperature control are proven.

Tie finish to functional need. Apply grinding, deburring, polishing to achieve roughness ranges (Ra ~3.2 to 0.8 μm) for sealing or low-friction surfaces on a part.

Volume planning and lights-out scalability

Choose machines/workflows for your volume. For repeat high-volume runs, consider 24/7 lights-out cells and bar-fed setups to keep throughput steady and speed changeovers.

Quality controls and in-process checks

Document acceptance criteria, GD&T, and FAI. In-process checkpoints identify variation early and maintain repeatability during production.

  • Use CAD/CAM simulation to refine toolpaths and limit rounding error.
  • Verify ISO 9001/AS9100 and metrology capability.
  • Record sampling/control plans per end-use needs.

The team reviews drawings against these benchmarks and recommends measurable requirements to de-risk sourcing decisions. This approach stabilizes production and improves on-time delivery.

Processes & Capabilities for Precision

Integrating 5-axis, live tooling, and finishing enables delivery of ready-to-assemble parts with fewer setups and minimal handling.

5-axis milling and setup efficiency

Five-axis systems with automatic tool change handles five sides in one setup for complex features. VMCs and HMCs provide drilling and chip evacuation. Result: fewer re-clamps, better feature accuracy.

Turning, live tooling, and Swiss methods

Live-tool lathes can remove material and add cross holes or flats without additional operations. Swiss turning is often used for slender/small parts in volume runs with tight runout.

EDM / Waterjet / Plasma & finishing

Wire EDM shapes hard metals and fine forms. Waterjet is ideal for heat-sensitive stock, and plasma provides fine cuts on conductive metals. Final grinding, polishing, blasting, and passivation improve finish and corrosion resistance.

Capability Best Use Buyer Benefit
Five-axis & ATC Complex features on many faces Fewer setups, faster cycles
Live tooling & Swiss turning Small, complex high-volume Lower cost at volume, tight concentricity
EDM / Waterjet / Plasma Hard or heat-sensitive shapes Accurate contours, less rework

UYEE-Rapidprototype.com pairs these capabilities and process controls with disciplined machine maintenance to protect repeatability and schedules.

Material Choices for Precision: Metals and Plastics

Material selection shapes whether a aluminum CNC machining design hits functional and cost/schedule targets. Early selection reduces iterations and helps align manufacturing strategies with performance targets.

Metals: strength, corrosion, and thermal control

Popular metals: Aluminum 6061/7075/2024, steels like 1018 and 4140, stainless steels 304/316/17-4, Titanium Ti-6Al-4V, copper alloys, Inconel 718, and Monel 400.

Evaluate strength/weight vs. corrosion to meet the use case. Use rigid fixturing and thermal management in machining to hold tight accuracy when cutting heat-resistant alloys.

Engineering polymers: when and why

ABS, PC, POM/Acetal, Nylon, PTFE (filled/unfilled), PEEK, PMMA serve many applications from housings to high-temperature seals.

Polymers are heat sensitive. Slower feeds and conservative spindle speeds protect dimensional stability and surface finish on the part.

  • Weigh metals by strength, corrosion, cost to select the right class.
  • Select tools and feeds for alloys such as Titanium and Inconel to remove material cleanly and extend tool life.
  • Apply plastics where low friction or chemical resistance is needed, tuning parameters to prevent warp.
Class Best Use Buyer Tip
Aluminum/Brass Light housings with good machinability Fast cycles; check temper and finish
Steels/Stainless Structural, corrosion resistance Plan thermal control and hardening steps
Titanium & Inconel High-strength, extreme service Slower feeds; higher tooling cost

UYEE-Rapidprototype.com helps specify material and testing coupons, document callouts (temp range, coatings, hardness), and match machines and tooling to the selected materials. Guidance shortens validation and reduces redesign.

CNC Precision Machined Parts

Good CAD and optimized toolpaths cut iteration time and maintain tolerances.

UYEE-Rapidprototype.com turns CAD into CAM programs that produce optimized G/M code with simulated toolpaths. That workflow reduces rounding errors and lowers cycle time while keeping accuracy tight on the workpiece.

Design-for-Manufacture: toolpaths and fixturing

Simplify features, pick stable datums, and align tolerances to function so inspection remains efficient. CAM-driven toolpath strategy and cutter selection cut non-cut time and wear.

Employ rigid holders, robust fixturing, and ATC to reduce changeover time. Early collaboration on threads, thin walls, and deep pockets reduces risk of deflection and finish problems.

Industry applications: aerospace, automotive, medical, electronics

Applications range from aerospace structural components and turbine blades to automotive engine items, medical implants, and electronics heat sinks. Each sector has specific traceability and cleanliness requirements.

Managing cost: time, yield, waste

Efficient milling strategies, better chip evacuation, and nesting for plate stock cut scrap and material cost. Prototype-through-production planning keeps fixtures and machines consistent to protect repeatability as volumes scale.

Focus Buyer Benefit When to Specify
DFM-driven design Faster approvals, fewer revisions Early quoting
CAM toolpath & tooling Lower cycle time, higher quality Before production
Material nesting & bar yield Less waste, lower cost During production

The team serves as a DFM partner, offering CAD/CAM optimization, fixturing guidance, and transparent costing from prototype through production. This disciplined system keeps projects predictable from RFQ to steady-state FAI.

Final Thoughts

In Closing

Consistent control of tolerances and workflows translates intent into repeatable outputs for demanding industries. Process discipline and robust controls with proper equipment enable repeatability for critical parts across medical, aerospace, automotive, electronics markets.

Proven capabilities and clear requirements, backed by data-driven inspection, protect quality while supporting tight schedules and cost goals. Advanced milling, turning, EDM, waterjet, and finishing—often used together—cover a wide range of part families and complexity levels.

Material choices from Aluminum/stainless to high-performance polymers ought to fit function, budget, and lead time. Thoughtful tool choice, stable fixturing, and validated programs reduce cutting time and variation so each workpiece meets spec.

Share drawings and CAD for a DFM review, tolerance confirmation, and a plan to move from prototype to production with predictable outcomes. Contact UYEE-Rapidprototype.com for consultations, tailored quotes, and machining services that align inspection, sampling, and acceptance criteria with your business objectives.

Related: CNC Milling Houston: Retrofit and Upgrade Options for Older Machines

Fall Arrest Vs. Work Positioning In Harness Systems

Rope Access Works — Flux Professional Services in Singapore

In Singapore, buildings frequently lower exterior maintenance costs by as much as 40% when they implement rope access. This is due to its speedier setup and lower labour hours.

Flux Solutions offers specialized https://flux.com.sg solutions for high-rise upkeep throughout Singapore. Our IRATA-qualified team completes façade cleaning, inspections, and repairs in complex locations. All work is carried out with minimal disruption to occupants and street traffic.

Clients trust Flux – Rope Access works for precision, safety, and clear accountability. Each project comes with full insurance coverage and a workmanship warranty. As a result, rope access in Singapore is a dependable option for owners and facility teams.

Go to Flux.com.sg to book a free assessment or see timelines, safety credentials, and our service guarantee.

Highlights

  • Certified rope access services from Flux Solutions are tailored for Singapore high-rise assets.
  • Compared with scaffolding, rope access cuts setup time and cost.
  • IRATA-trained technicians ensure compliance, safety, and professional standards.
  • Offerings span façade cleaning, inspections, painting, and repairs in hard-to-reach zones.
  • Full insurance and workmanship warranty provide peace of mind for property teams.

Flux - Rope Access works

Rope Access Overview and Advantages for Singapore Buildings

For Singapore buildings, rope access offers a low-footprint and efficient way to reach tall or confined areas. Trained technicians use harness systems, climbing gear, and certified anchor points. It avoids scaffolds or boom lifts, thereby reducing setup time and the urban work footprint.

Core Principles and Definition of Rope Access

Rope access ensures safety at height through two-point redundancy and fall-arrest backups. All equipment is inspected before work, following documented procedures. Anchors, ropes, and rescue plans are handled by trained technicians. The method enables precise positioning on facades, towers, and curved surfaces where conventional access is impractical.

Why rope access is preferred over scaffolding and boom lifts in urban settings

Scaffolding often requires street closures and long erection periods. Boom lifts need clear ground access and space for operation. These constraints are bypassed with rope access. Rapid mobilization from rooftops or balconies helps avoid blocking pedestrian walkways. That speed helps managers and tenants maintain daily operations.

Key Benefits: Faster Setup, Lower Cost, Minimal Disruption

Faster setup means projects start sooner and finish quicker. Reduced materials and labour usually mean lower costs. Minimal disruption matters for mixed-use sites, malls, and condos across Singapore. When combined with targeted work plans, rope access solutions deliver high value with limited disturbance to occupants.

Applications suited to Singapore’s high-rise and constrained sites

Rope access is ideal for façade cleaning, paint touch-ups, waterproofing, structural inspections, and signage installation on high-rises. Narrow lanes, conserved shophouses, and tight estates benefit where scaffolds are constrained. Whether for urgent fixes or scheduled works, rope access teams keep projects on track with flexible, safe methods.

Common Task Traditional Method Rope Access Advantage
Façade cleaning Scaffolding or gondola hire, long setup Rapid mobilization, minimal street footprint, reduced cost
Painting and coating Long scaffold durations, heavy material staging Accurate access on curved areas, leaner staging
Inspections and diagnostics Reliance on cranes/lifts with limited reach Reach into confined zones, faster technician reporting
Repair in narrow alleys Temporary road closures or complex rigging No road closure, minimal public disruption

Flux – Rope Access works

Flux Solutions leads in high-access maintenance across Singapore. Offerings span façade cleaning, exterior painting, waterproofing, signage installation, wall repairs, and inspections. Free assessments and quotes help clients choose the right rope access services for tight urban conditions.

Company profile and service focus

With 10+ years’ experience, Flux Solutions provides flux – rope access works across varied structures. The team blends field experience with diagnostic tools to drive efficient repairs. Planning respects tenant access and site constraints.

Certifications and compliance

At Flux Solutions, IRATA-certified technicians follow international rope access standards. The firm is BCA-registered and holds bizSAFE Level 3. Such credentials ensure reliable planning and compliance on complex projects.

Service Promise & Assurances

Clients enjoy full insurance coverage for works at height and a workmanship warranty on completed jobs. Flux Solutions boasts a documented safety record with zero major incidents. Project updates, quick turnarounds, and flexible schedules help minimize disruption.

Flux Solutions: Rope Access Services

Flux Solutions specializes in multiple rope access services tailored to Singapore’s urban landscape. Technicians perform high-facade work using meticulous safety protocols and tailored methods. The approach delivers targeted maintenance while minimizing downtime and disruption.

Facade cleaning and high-rise exterior maintenance

We maintain cladding, glass, and metal joints through professional facade cleaning. We remove pollutants, bird soiling, and biological growth to slow material deterioration. Regular programs maintain appearance and defer costly repairs.

External painting, coating, and waterproofing at height

We apply protective coatings and paints without full scaffolds to accelerate completion. Utilizing access-rated techniques, we apply sealants and membranes in hard-to-reach areas. This ensures waterproofing at height, protecting structural elements and finishes from water damage.

Wall repairs, signage installation, and specialized installations

Our technicians perform precise wall repairs, including grout and render work. Installation and maintenance of signage and exterior lighting proceed with minimal disruption. Thanks to rope access, we reach areas cranes or lifts can’t.

Inspection services and diagnostic assessments for efficient repairs

Our IRATA-trained technicians conduct thorough inspections to identify defects swiftly. They guide repair scope and materials to avoid unnecessary tasks. Detailed inspection outputs inform maintenance plans and lifecycle budgeting.

All our work adheres to strict safety standards, employs certified equipment, and includes a free consultation. We provide site-specific recommendations to ensure the best outcomes for our clients.

Safety & Certification Standards for Rope Access

On every project, Flux Solutions prioritizes safety at height. Teams follow rigorous protocols before any rope is secured. Clear communication with managers and detailed risk-minimizing plans are included.

IRATA certification underpins our technicians’ competence. They undergo structured courses, practical exams, and regular re-assessments. Training covers rigging, fall arrest, backups, and rescue drills, which significantly improve real-world performance.

On-site protocols demand adherence to industry standards. Certified harnesses, helmets, anchors, and redundant ropes are required. Daily toolbox talks and site-specific method statements are essential to address hazards proactively.

We keep meticulous logs for inspections, near-misses, and audits. Such logs are integral to our active risk management program. They help refine procedures and reduce the occurrence of repeat issues. Ongoing reviews ensure compliance with local regulations and client expectations.

Insurance coverage is a critical complement to our technical safeguards. It protects both personnel and third parties, reinforcing our commitment to workplace safety. Our bizSAFE Level 3 practices further solidify this commitment, making rope access technicians accountable and ensuring safer work sites.

Project Planning & Execution for Rope Access

Flux Solutions starts every project with a detailed site assessment and a free consultation. We assess access points, anchors, hazards, and equipment. This step confirms feasibility and provides a clear, no-obligation quote.

Site assessment and free consultation process

The site assessment measures dimensions, checks anchor integrity, and notes tenant flow. Data informs the project’s risk registers and method statements. A detailed summary outlining scope and safety is provided to clients.

Project planning: scope, timeline, and minimal disruption strategies

Planning defines clear scope and a phased timeline. Tasks, sequences, personnel, and permits are outlined. Off-peak scheduling is used to minimize tenant disruption. The use of rope access solutions reduces the ground footprint compared to scaffolding.

From Setup to Warranty Support

Setup proceeds swiftly. Technicians install anchor points, verify redundancy, and conduct pre-task risk assessments. Work can begin within days of the assessment. Ongoing monitoring maintains safe execution and quality control.

Regular progress reports and direct communication keep building management informed. All completed work includes a workmanship guarantee and post-work warranty support. Final inspections and recommended maintenance plans are provided to safeguard asset value.

Cost, Timelines, and When to Choose Rope Access

For high-rise maintenance in Singapore, rope access can significantly lower costs and speed delivery. Understanding cost drivers, lead times, and a suitability checklist is essential for owners to choose between rope access, scaffolding, or mechanical lifts.

Cost Advantages

Rope access reduces scaffold setup and teardown costs. Expensive boom lift rentals are avoided and manpower needs are reduced. Compared with full scaffolds, Flux Solutions often delivers lower total cost and shorter downtime.

Lead Times & Rapid Response

Work typically begins within days after a site assessment. For urgent facade defects or safety hazards, rapid-response rope access teams can be mobilized quickly. This limits risk and visible damage. We offer flexible scheduling for deadlines and emergencies.

Is Rope Access Right? A Checklist

  • High-rise facades and tower faces
  • Curved or narrow elevations
  • Confined spaces, rooftops, and lane-facing walls
  • Signage at height, localized repairs, and paint or coating patches
  • Detailed inspections where scaffold is impractical

Limits of Rope Access

For heavy handling or long durations, https://flux.com.sg scaffolding or suspended platforms may be preferable. We recommend a free feasibility check to confirm the best method.

Decision factors for clients

Factor Rope Access Scaffolding/Lifts
Scale Ideal for targeted/localized tasks Better for large, whole-envelope works
Constraints Works well in narrow lanes and irregular facades May be restricted by street width and site logistics
Urgency Supports rapid response for quick fixes Longer setup, less suitable for urgent fixes
Budget Lower overall costs for small/medium jobs Higher from equipment and erection labour
Disruption Minimal disruption to occupants and street users Greater disruption from scaffold or lift staging

Use Flux Solutions’ site assessment to weigh these factors. The assessment produces a clear recommendation based on scope, urgency, budget, and disruption tolerance. It uses a practical suitability checklist tailored to Singapore’s built environment.

Conclusion

Flux Solutions excels at delivering rope access works for Singapore’s dense urban landscape. The IRATA-certified team provides services including facade cleaning, inspections, and exterior painting. They also complete waterproofing, wall repairs, and signage installs, all backed by full insurance and a workmanship warranty. This ensures efficient maintenance with minimal disruption to tenants and operations.

Rope access is distinguished by quick setup, cost efficiency, and a small footprint. These advantages make them perfect for Singapore’s high-rise buildings, narrow lanes, and tight rooftops. For urban maintenance, this method is a game-changer.

Owners, facility managers, and maintenance teams can secure a free site assessment and quote from Flux Solutions. We offer rapid-response options and expert advice on rope access suitability. Safety at heights is their top priority, with operations meeting IRATA standards. As a BCA Registered Contractor with bizSAFE Level 3, professional and compliant execution is ensured.

The Role Of Binders In The Metal Injection Molding Process

Metal Injection Molding in Singapore: Premium Solutions

Globally, Singapore leads in advanced manufacturing and precision engineering. With robust infrastructure and a highly skilled workforce, it’s an ideal hub for innovative solutions. Organizations like AMT have prospered, delivering advanced services for more than thirty years.

AMT specializes in metal injection molding (MIM), delivering high-quality, complex parts for high-volume production. Their integrated https://amt-mat.com/business/mim/metal-injection-molding approach covers everything from tooling to assembly, ensuring streamlined supply chains for clients worldwide.

Backed by certifications and strict quality standards, AMT has earned a reputation for reliability. Their global clientele spans industries, from automotive to medical devices. Singapore’s supportive ecosystem and AMT’s technical expertise underpin this success.

Key Takeaways

  • Singapore is a hub for advanced manufacturing and precision engineering
  • With 30+ years of experience, AMT leads MIM solutions
  • Integrated operations help maintain efficient supply chains
  • Quality standards and certifications strengthen credibility
  • Clients worldwide benefit from Singapore’s skilled talent

Introduction to Metal Injection Molding in Singapore

Innovation and precision define Singapore’s manufacturing landscape. Firms such as AMT have helped advance metal injection molding (MIM) technology. Founded in 1990, AMT has grown into a leader, integrating MIM with precision tooling, CNC machining, and 3D printing for end-to-end solutions.

A strategic location strengthens Singapore’s global distribution reach. This positioning lets AMT efficiently support medical, automotive, electronics, and industrial clients. AMT tackles fragmented supply chains to ensure seamless production and delivery of quality components.

The process of MIM involves combining fine metal powders with binders to create intricate parts. AMT’s expertise plus Singapore’s infrastructure position the company as a trusted partner for complex manufacturing. Continued focus on innovation and quality fuels success globally.

AMT

Understanding Metal Injection Molding (MIM)

Metal injection molding is an advanced process blending precision and efficiency. It allows for the production of complex, high-performance components with tight tolerances. Automotive, medical, and electronics sectors commonly adopt this method.

The MIM Process Explained

The mim process involves four key steps: mixing, injection, debinding, and sintering. Initially, fine metal powders blend with binders, creating a feedstock. This mixture is then injected into molds to form a green part, which holds the shape of the final component.

Afterward, the green part is debound to remove binders, yielding a brown part. Finally, the brown part is sintered at high temperatures to achieve its final density and strength. Sintering typically causes ~15% shrinkage, producing a near-net component with precise dimensions.

Key Components of MIM

The mim process relies on several critical components to ensure quality. Custom feedstock formulations match specific alloys, enabling material flexibility. The green part and brown part stages are essential for achieving the desired density and shape.

Final sintering is key to final durability and strength. Unlike traditional machining or plastic injection molding, MIM produces parts with intricate geometries and high material efficiency. As a result, industries that require precision and performance prefer MIM.

Why Choose Metal Injection Molding

Innovative manufacturing has transformed complex component production with exceptional accuracy. Notably, https://amt-mat.com/what-is-medical-manufacturing/ delivers advantages like high precision, flexible materials, and strong performance. These advantages make it the choice for industries needing intricate, durable parts.

High Precision and Tight Tolerances

Tolerances down to ±0.3% help ensure exact specifications. Surface finishes are smoother than 32 µin Ra, reducing the need for additional polishing. Thin-wall capability to 0.2mm lets AMT create intricate designs featuring complex geometry.

Versatile Materials and Strength

From stainless steel (for corrosion resistance) to dense tungsten alloys, material choices are broad. Functionality is enhanced through AMT’s In-Coring® and bi-material integration, reducing size and weight. This versatility allows for tailored solutions across industries, from medical devices to automotive components.

Significant cost savings are also achievable. By minimizing secondary machining and assembly, production is streamlined. For example, medical devices requiring biocompatible, sterilizable components benefit from these efficiencies. This combination of high strength, precision, and material flexibility makes the technique a game-changer in modern manufacturing.

Applications of Metal Injection Molding

The versatility of advanced manufacturing techniques enables the creation of highly specialized components across industries. From medical devices to automotive systems, these methods deliver precision and reliability. AMT leverages the technology to make critical parts that meet strict standards.

Medical and Surgical Instruments

In the medical field, precision is paramount. AMT produces stainless steel endoscopic graspers and robotic surgical tools that meet rigorous biocompatibility standards. These components support minimally invasive procedures, protecting patients and improving efficiency.

MRI parts and disposable instruments are other medical applications. High strength and sterilizability make them ideal for this process. With tungsten alloys, AMT enables imaging-device shielding, highlighting the technology’s adaptability.

Industrial and Automotive Applications

Automotive applications benefit from precise, durable parts such as fuel injectors and sensor housings. These components drive performance and reliability. AMT’s transmission gears and seatbelt mechanisms underscore suitability for high-stress use.

Industrial settings rely on high-pressure valves and wear-resistant automation parts. These items ensure smooth operations in demanding conditions. Producing complex geometries with tight tolerances makes the method preferred for industrial applications.

Sector Use Cases
Medical Devices MRI components, endoscopic graspers, robotic instruments
Automotive Fuel injectors, sensor housings, transmission gears
Industrial Automation wear parts, high-pressure valves
Consumer Electronics Smartphone hinges, 5G heat sinks

The applications of this technology span medical to automotive innovations. Its ability to produce high-quality, intricate parts ensures its relevance across diverse industries. AMT’s pursuit of excellence drives global delivery of tailored solutions.

Why MIM in Singapore Makes Sense

Advanced manufacturing thrives in Singapore, offering unparalleled solutions for global industries. The city-state’s strong infrastructure and skilled talent create a hub for precision engineering and innovative production. Companies like AMT leverage these advantages to deliver high-quality results.

Singapore’s strong IP protection laws ensure the security of proprietary designs and processes. AMT’s compliance with FDA and ISO 13485 standards further enhances its credibility, making it a trusted partner for industries like medical devices and automotive.

Advantages include English-speaking engineers, rapid turnaround, and AMT access to a busy global port. They streamline logistics and support timely delivery of components worldwide.

AMT’s co-development process optimizes part geometry and material selection, ensuring efficiency and cost-effectiveness. Design-for-MIM support and rapid prototyping at an ISO-certified facility help reduce time-to-market.

Quality assurance remains paramount at AMT. Components pass stringent in-house tests before delivery. That commitment reinforces AMT’s reliable and precise reputation.

For project consultations, contact AMT at +65 6865 5700 or via 5700 email. The team stands ready to assist with tailored manufacturing solutions.

Materials for MIM

Precision and durability depend heavily on the chosen materials. To meet diverse needs, AMT uses a wide range of ferrous and non-ferrous alloys. Such materials help components perform reliably in demanding environments.

Ferrous and Non-Ferrous Alloys

With tensile strengths up to 1400 MPa, ferrous alloys such as 17-4 PH stainless steel provide high strength. Soft magnetic alloys are widely used for unique magnetic properties. Non-ferrous options include MP35N, known for MRI safety, and tungsten-copper blends for thermal management.

Expertise also covers advanced alloys: F75 cobalt-chrome for implants and Inconel 718 for aerospace. Providing corrosion resistance and high-temperature stability, these alloys suit critical components.

Custom Feedstock Solutions

Custom materials are tailored to specific applications. Tungsten content (90–92.5%) is tuned for radiation shielding as needed. Nickel-free stainless steel and other biocompatible options are essential for surgical tools and medical devices.

AMT’s material testing protocols ensure traceability and quality. Each batch undergoes rigorous checks to meet standards. This level of commitment helps guarantee component reliability.

Alloy Class Example Applications
Iron-Based Alloys 17-4 PH stainless steel, soft magnetic alloys
Non-Ferrous F75 cobalt-chrome, MP35N, tungsten-copper
Customised Blends Tungsten-adjusted blends, nickel-free stainless steel

Future Trends in MIM

New trends in advanced production are redefining standards. At the forefront, companies like AMT integrate mim technology with 3D printing and AI optimization. Innovations like these enable smarter and more efficient manufacturing solutions.

Trends include medical-tech miniaturization and automotive lightweighting in design. R&D at AMT focuses on nano-powders for finer features and faster sintering. Sustainability is also a priority, with binder recycling and energy-efficient debinding techniques reducing environmental impact.

Digital twin technology is revolutionizing quality monitoring. By creating virtual replicas of physical components, manufacturers can detect defects in real-time, ensuring higher precision and reliability. This approach is particularly valuable for industries like 5G infrastructure and electric vehicle (EV) components, where demand is rapidly increasing.

Evolving industries will likely expand adoption of mim technology. Unmatched precision for complex, high-performance parts makes it vital for future production. AMT’s commitment to innovation ensures they remain a trusted partner in this dynamic landscape.

Final Thoughts

AMT has delivered precision manufacturing solutions for over three decades. They set benchmarks for quality and reliability through end-to-end capabilities and material innovation.

Leveraging Singapore’s robust manufacturing ecosystem, AMT ensures seamless production and timely delivery. Expertise spanning medical to automotive makes them a preferred global partner.

For inquiries, contact AMT’s team at +65 6865 5700 or via 5700 email. For time-sensitive projects, they provide quick-response prototyping to meet needs efficiently.

A commitment to customer-centric partnerships and unmatched quality remains at AMT. Count on them for tailored solutions that drive success.

Material Selection Tips from AMT’s High Precision Plastic Injection Molding Experts

Precision Plastic Injection Molding by AMT Singapore.

A tiny medical component can demand extreme accuracy while still being mass-produced—did you know? That level of detail is essential across medical, automotive, and electronics applications. They look for dependable partners in Singapore.

With roots in 1990, AMT brings over three decades of partnership to manufacturers. Their capabilities span precision tooling, plastic molding, micro molding, and CNC machining. This helps lower the number of suppliers needed and get products out faster.

AMT works in 30 countries and has top-notch high precision plastic injection molding: AMT facilities. Safety and reliability anchor their manufacturing, notably for medical devices. Their focus on detailed plastic parts and high precision plastic injection molding makes them a go-to in Singapore for quality and consistency.

What is Precision Plastic Injection Molding and why it matters in Singapore

This process provides high throughput while maintaining consistent quality. It involves melting plastic pellets and injecting them into molds under high pressure. It enables complex geometries and fine features beyond many alternative processes.

Definition and core principles of injection molding

This process combines material choice, mold design, and machine settings. The type of resin used impacts the strength and flow of the part. Precision comes from tooling with correct venting, gating, and cooling. Precise machine settings lock in repeatable production.

AMT - high precision plastic injection molding

Industry relevance for Singapore manufacturers and OEMs

Singapore’s medical, electronics, and automotive sectors require highly reliable components. By combining tooling with molding, AMT streamlines builds. That helps Singapore firms meet regulations and protect IP.

Key Metrics: Tolerance, Cycle Time, Yield

Tight tolerances up to ±10 µm are achievable with careful process and tool management. Cycle-time reductions via advanced cooling reduce cost without sacrificing quality. Improved yields result from automation and early defect detection, minimizing the need for rework.

Performance Metric Typical Target Manufacturing Impact
Tolerance ±10–100 µm Controls fit/function and assembly consistency in precision parts
Cycle Time 2–60 seconds per shot Drives throughput, lead times, and unit economics at volume
Yield ~95–99.9% Reduces scrap/warranty risk and boosts efficiency
Traceability Batch→Serial Supports regulatory audits and warranty claims for medical and automotive parts
Run Customization Low- to high-volume runs Supports tailored solutions via DFM and custom manufacturing

Choosing precision molding points to integrated quality-driven production. Singapore firms gain cost control, vendor reduction, and quicker launches. A practical path to remain competitive.

precision plastic injection molding – AMT

AMT serves as a key partner for managing complex supply chains. It combines tooling, molding, and assembly to shorten lead times. Clients get less waiting, more doing, and a single point of contact.

AMT’s positioning as a strategic contract manufacturing partner

Across medical, automotive, and electronics, AMT delivers integrated solutions. It helps original equipment manufacturers (OEMs) and contract manufacturers bring designs to life. Teams trust AMT for end-to-end reliable support.

AMT Experience and Global Footprint

Three-plus decades of innovation fuel AMT’s growth. Their customer base spans over 30 countries. Roughly 350 employees power product development, precision molding, and complex assemblies.

Holding 29 patents and 15 inventions, AMT underscores innovation—especially in microfluidics and automotive components.

Precision-Enabling Certifications: ISO 9001, ISO 13485, IATF 16949

Strong quality and regulatory credentials support customer demands. ISO 9001 certification demonstrates adherence to quality management systems. The ISO 13485 certification means it meets the stringent requirements for medical device production. IATF 16949 ensures alignment with automotive standards for traceability and defect prevention.

Collectively, these credentials position AMT as a precision molding leader. For high-precision molding or custom plastic manufacturing, AMT is a go-to partner. Capabilities scale while ensuring compliance across the product lifecycle.

Specialized Molding Capabilities & Technologies at AMT

High-precision tooling and molding for medical/auto/electronics define AMT Singapore. Class 10k and 100k cleanrooms support production. That minimizes contamination and supports intricate micro-scale programs.

For diagnostics and wearables, micro molding is ideal. AMT runs advanced micro-molding injection presses. They produce highly accurate, consistent parts—even with complex geometries.

AMT’s high-cavitation precision molding drives volume production. Tooling is engineered for uniform thermal control and precise gate placement. This guarantees a consistent surface finish and uniform dimensions throughout large batches.

AMT’s multi-shot molding techniques offer enhanced design flexibility. Overmolding/2K supports seals, color accents, and integrated hinges. Additionally, auto insert molding incorporates metal or ceramic inserts in one go, ensuring robust connections.

Rapid heat and cool tooling technologies are utilized to decrease cycle times and heighten the aesthetic appeal of complex components. Overmolding is fundamental for adding soft elastomers to hard bases. Each method demonstrates AMT’s commitment to high-precision plastic injection molding for industries with strict regulations.

AMT maintains exacting standards through process control and in-house CNC machining. It allows rapid tooling refinements. By integrating micro molding, high cavitation precision molding, and multi-shot techniques, AMT aids designers in moving from prototypes to production efficiently and cost-effectively.

Materials & Sustainability Options at AMT

Material choices weigh performance alongside eco-friendliness. Early material selection aligns with sector-specific needs (medical/auto/electronics).

Common thermoplastics and specialty polymers

ABS, PC, and nylon suit durable parts. PEEK and Ultem are great for jobs requiring resistance to heat and maintaining shape. Unique requirements drive the use of specialty polymers.

Sustainable Material Options

AMT adopts recycled plastics when appropriate. Reclaimed resins reduce footprint without sacrificing performance in many cases. They also consider biodegradable materials like PLA and PHA for jobs where they fit the rules and needs.

Sector-Specific Material Considerations

Medical applications need biocompatible, sterilizable, fully traceable materials. AMT enforces strict rules in cleanrooms to ensure patient safety.

In the auto industry, materials must withstand heat, chemicals, and shaking. AMT evaluates durability and thermal behavior.

Electronics require low outgassing, flame resistance, and dimensional stability. Materials influence function, assembly outcomes, and appearance.

Environmental targets lead AMT to account for lifecycle and recycling. Their expertise in tooling and materials makes it possible to use recycled or biodegradable plastics without losing quality.

AMT’s End-to-End Workflow: From Design to Delivery

AMT transforms CAD concepts into finished parts with precision at each stage. They begin by reviewing designs and checking if they can be made reliably. Engineers work to make sure parts can be made quickly and work well by improving design features like thickness and rib placement.

DFM & Design

Computer simulations predict design performance. Early validation reduces revisions and cost. Goal: ensure molded parts match the initial design closely.

Tooling and mold fabrication

Precision molds are cut using 5-axis CNC and advanced tooling. Strict procedures and robust steels yield long-life molds.

Cleanroom Assembly & Handling

Parts undergo assembly, welding, and rigorous inspection after molding. They have special clean rooms for assembling parts that must be kept free from contaminants.

Stage Key Activities Primary Benefits
CAD & DFM Simulation, wall optimization, tolerance strategy Reduced revisions and predictable molding
Toolmaking 5-axis CNC, EDM/wire-cut, precision grinding High-precision molds, long life, consistent cavities
Injection molding Micro and standard presses, process validation Repeatability, low scrap, controlled cycles
Assembly & inspection Robotics, cleanroom handling, traceable inspection Audit readiness, sterility, full traceability

End-to-end in-house work shortens wait times and simplifies execution. One owner across stages boosts reliability and lowers cost from design to production.

With sophisticated molding, they deliver parts tuned to your needs. Parts serve healthcare, auto, and electronics in Singapore and the wider region.

Ensuring High Precision: QA and Testing

AMT Singapore integrates tooling, molding, assembly, and inspection. This approach helps track each part from start to finish and meets tough demands for medical and automotive parts. Teams follow ISO 13485/IATF 16949 methods to keep steps clear and repeatable.

In production, real-time data is captured. Sensor data drives quick corrections and efficiency gains.

Robotic inspection checks many parts quickly and accurately with controlled force/lighting. Inspection data maps to genealogy for faster issue resolution.

Dimensional checks are key; metrology confirms tiny features accurately. Results support batch traceability and performance understanding.

Tracking goes right back to materials used, with AMT recording everything. That level of detail supports FDA/EU regulatory compliance.

ISO 13485 and IATF 16949-aligned systems cover design, risk, and suppliers. Regular audits and strict procedures keep quality high.

Applications & Use Cases AMT Serves in Singapore

Across Singapore industries, AMT moves programs from prototype to volume effectively. Vertical integration and cleanrooms make them a top choice for medical device manufacturing and quality plastic products.

AMT partners with medical teams on microfluidics and single-cell devices. Small optical parts with tight tolerances and clarity are produced under ISO 1345-aligned cleanroom processes to reduce contamination risks.

Automotive firms rely on AMT for critical parts like connectors that need to meet IATF 16949 standards. These parts are crucial for fuel systems, safety housings, and connectors—designed for durability and traceability.

Electronics companies get micro housings, connectors, and components from AMT for both consumer and industrial items. Their molding techniques maintain consistency to electro-mechanical specs.

Here’s a concise industry-by-industry view of applications, requirements, and strengths.

Sector Applications Requirements Strengths
Medical Microfluidic chips, single-cell cartridges, lens-care inserts Biocompatibility, low particulate, optical clarity, regulatory traceability ISO 13485, cleanrooms, precision tooling
Automotive Connectors, fuel fittings, safety housings Durability, vibration resistance, dimensional stability IATF workflows, robust materials, traceable production
Electronics Micro housings, precision connectors, EMI shields Tight tolerances, surface finish, repeatable cycle-to-cycle accuracy High-cavitation molding, multi-shot capability, in-line inspection

Manufacturers in Singapore favor AMT for high-precision plastic components that can scale. OEMs find AMT’s comprehensive services cut time-to-market and protect design integrity.

Advanced Techniques & Industry 4.0 Integration

Singapore manufacturers are moving to interconnected cells, leveraging 3D metal printing and precision toolsets with digital workflows. This makes new manufacturing methods work for big and small production.

Smart molds monitor temperature/pressure and self-adjust in real time. This quick fix reduces stoppages and improves surface looks.

Robots standardize handling/QC, ensuring early good parts and reducing manual intervention.

Data analytics flags small issues early; process tweaks based on historical/live data keep quality consistent.

Innovations in molding and sensor control make manufacturing faster while keeping quality. Dashboards surface KPIs for quick informed decisions on the floor.

Research and strong property rights support these methods. With patents in metal powders and tools, there’s a deep commitment to new methods, driving better results from advanced manufacturing and Industry 4.0.

Choosing AMT for custom plastic manufacturing services in Singapore

AMT offers a seamless service from tooling, molding, to shipping, decreasing waiting times and easing supplier oversight. It’s perfect for manufacturers and OEMs in Singapore who want trustworthy custom plastic production.

Single-Source Contract Manufacturer

Single-source partners reduce handoffs and keep quality consistent. AMT has its own toolrooms and presses, ideal for clients in the medical, automotive, and electronics sectors.

IP protection and regulatory experience

Clients in regulated fields need strong IP protection and clear compliance methods. AMT follows strict protocols for managing designs and molds safely and is experienced with US FDA and EMA standards, ensuring safe and confident product launches.

Proof of Capability

AMT has earned respect through various certifications like ISO 9001 and ISO 13485, plus patents and awards for engineering and manufacturing.

Core Capability What it delivers Why It Matters
Integrated tooling and molding Faster validation cycles and fewer quality gaps Cuts time-to-market for precision parts
Assembly + Supply-Chain Integration End-to-end logistics and vendor management Streamlines production and lowers inventory risk
IP protection protocols Secure custody and controlled access Preserves competitive advantage for customers
Regulatory Compliance Processes aligned with FDA, EMA, and industry norms Enables smoother approvals for regulated parts
Technical Credentials Certifications, patents, and documented inventions Shows reproducible production excellence

Working with AMT means teams get to use effective molding strategies and deep process understanding. Asia-wide connections support growth and resilient supply lines.

Choosing AMT as a custom plastic manufacturing partner is a smart move. They protect IP and bring the right credentials.

To Summarize

For Singapore manufacturers, AMT’s integrated model and multi-disciplinary approach provide a strong foundation. Since 1990, AMT has integrated tooling, molding, assembly, and supply networks—reducing wait times and simplifying complex supply chains. That one-stop model makes AMT a top OEM choice for complex components.

For high-precision injection molding, AMT stands out. Advanced methods—micro molding, multi-shot—ensure reliable parts for medical/auto/electronics. Industry 4.0 integration minimizes waste and tightens precision.

AMT’s commitment to quality is proven through their ISO 9001, ISO 13485, and IATF 16949 certifications, cleanroom capabilities, and growing patent list. Technical skill plus supply-chain efficiency make AMT a key Singapore partner for custom plastic parts.

Automation in Compact Fiber Unit Packing

FTTH Drop Cable Production: Step-by-Step Manufacturing Process

Surprising fact: in excess of seventy percent of U.S. broadband rollouts now rely on fiber networks that need tight manufacturing control to achieve required performance.

Shanghai Weiye OFC Equipment runs end-to-end fiber secondary coating line manufacturing, from sourcing brand fibers like Fujikura or Corning SMF-28e to complete test reports that deliver 100% QA.

Our drop cable designs fit aerial, underground, and direct burial installation, with LSZH, polyvinyl chloride (PVC), and PE jacket options and configurations from 1–4 cores. We supply OS1/OS2 and OM2–OM4 grades plus ITU-T G.652D and ITU-T G.657 variants, Pantone sheath colors, and logo printing.

Automation and precision equipment keep line speed steady and repeatability high. Typical lead times are 4–5 days for orders < 100 km and 7–10 days under 500 km, with an min. order of 1 km and warranty for free replacement on quality issues.

Read on to see how materials, testing, and support combine to lower lifecycle cost and align the product to your network needs.

  • Shanghai Weiye OFC Equipment provides full manufacturing with lab validation for U.S. deployments.
  • A range of jacket options and fiber grades support different install environments.
  • Automated lines and machines deliver stable quality and stable optical performance.
  • Fast lead times, low MOQ, and brand fiber options support reliable procurement planning.
  • Comprehensive test reports and warranty back product reliability and compliance documentation needs.

FTTH Manufacturing Expertise by Shanghai Weiye OFC Equipment

When schedules and performance count, Shanghai Weiye OFC Equipment provides customized drop cables with complete test documentation.

As a focused supplier and manufacturer, Shanghai Weiye OFC Equipment combines purpose-built equipment with stringent material control. We offer customized service and products for residential/MDU deployments. Every order comes with 100% quality assurance and full test reports.

Our lab conducts high-temperature, salt-fog, and vibration testing to validate durability. Jacket options cover LSZH, PVC, and PE. Designs offer flat bow-type and self-supporting styles and use brand fibers such as Fujikura and Corning SMF-28e.

FTTH cable production line

  • Controlled production lines and production checks for shipments with audit trails.
  • Technical support for specs, trials, and ramp to volume.
  • Modern fixturing and calibration reduce variability so every cable matches operator specs.

FTTH cable production

At Shanghai Weiye OFC Equipment, manufacturing steps are built around network requirements, pairing brand fiber choices with disciplined test flows.

Optical fiber selection and brand options

We select Fiber coloring machine to bend radius, loss, and deployment type. Options include OS1, OS2, OM2–OM4 and G.652D and G.657.A1/A2 per ITU-T. Brand fibers such as Fujikura and Corning SMF-28e are offered to meet procurement standards.

Integrating Strength Members

Strength members employ dielectric FRP or metallic steel wire. FRP is preferred where non-conductivity is necessary. Steel wire provides tensile strength for long-span aerial runs and bonding/grounding needs.

Extrusion & Process Control

Jacket options include LSZH for flame/smoke safety, PVC for flexibility and ease of handling, and PE for outdoor UV and moisture resistance. Closed-loop control of extruder temperature and capstan speed stabilizes line speed and critical dimensions.

Member FRP Metallic Steel
Use case Electrical isolation High-tension aerial runs
Key benefit Lightweight, inert High strength
Installation note Easier terminations Bonding/grounding required

Inline and final testing

Inline geometry and concentricity checks operate in-line. Final optical tests verify attenuation and reflectance. Each order includes a 100% test report and lab results from high heat, salt-spray, and vibration trials to qualify field handling and drop terminations.

Typical lead times are 4–5 days for < 100 km and 7–10 days for < 500 km. Material lot records and first-article approvals support traceability and compliance for U.S. projects.

FTTH drop cable types and structures we manufacture

Shanghai Weiye OFC Equipment offers a compact portfolio of drop designs that fit indoor risers and long aerial runs. Each option pairs tested materials with geometry tuned for field termination and consistent optical performance.

The flat bow-type drop keeps a small footprint for risers/ducts. It keeps bend loss low for simple routing in hallways and MDUs.

Self-Supporting Aerial Designs

Self-supporting FTTH drop designs use a messenger element to handle tension. Choose FRP (dielectric) for non-conductive runs or steel messenger when bonding/grounding and higher tensile strength are required.

Core Layouts and Strength Members

We offer both dielectric and metallic strength member configurations to meet safety/EMI requirements. Center loose tube and unitube flat types balance crush resistance and fiber ribbone line for quick termination.

Jackets for Indoor/Outdoor

Jacket choices include LSZH for indoor flame/smoke compliance and PE for outdoor UV and moisture resilience. Each family is qualified for mechanical/optical performance before shipment.

Type Best use Strength member Sheath
Bow-type flat Indoor risers, MDUs Dielectric FRP Low-smoke zero-halogen
Self-supporting (aerial) Overhead spans FRP/Steel PE
Central loose-tube Higher-count builds Dielectric FRP LSZH or PE
Flat unitube Low count, quick strip FRP or steel LSZH or PE

Equipment Ensuring Quality and Throughput

Automation with sensor feedback at Shanghai Weiye OFC Equipment cut manual handling and increase throughput for drop patch preparation.

Our production line integrates automated machines that cut/strip drop cords to increase output and reduce operator variability.

The CLX-BPO2 auto-stripping machine runs under PLC and photoelectric control. One cycle is ~1.5 s, giving ~20 terminals per minute in production.

Auto Cut & Strip Capabilities

The equipment strips LSZH and PVC jackets and trims FRP or steel strength members to precise reserved lengths. Cylinder-driven actuators provide quick, repeatable motion and minimize downtime.

Closed-Loop Control for Repeatability

PLC logic and photoelectric sensors give exact positioning and feedback control. Inline checks update SPC charts so operators can adjust drifts before out-of-control conditions occur.

Feature Capability Benefit
CLX-BPO2 Auto-strip, ~1.5 s cycle High throughput
Actuation Pneumatic cylinders Fast/reliable motion
Material handling LSZH/PVC; FRP/steel Accurate stubs, clean terminations
Control PLC/photoelectric with in-line SPC Consistent quality, lower rework
  • Auto scrap ejection and ergonomic feeders keep the line clean.
  • PCPs capture calibration intervals and critical parameters.
  • Combined machines, fixtures, and trained staff support FTTH volume targets without sacrificing accuracy.

CLX-BPO2 auto-stripping machine capabilities in our line

The CLX-BPO2 brings industrial-grade stripping and trimming to our line, reducing cycle time while keeping prep consistent.

Shanghai Weiye OFC Equipment uses the CLX-BPO2 to increase throughput and standardize prep quality. The unit runs at an approximate cycle time of 1.5 seconds, producing around 20 preps per minute in production.

PLC and photoelectric control deliver exact detection and repeatable actuation. That control helps keep strip lengths and reserved strength stubs within tight tolerances.

Line Speed

Typical operation speed is 1.5s per cycle. This translates to steady throughput under normal production conditions.

Supported jacket and reserved strength lengths

The CLX-BPO2 handles LSZH/PVC with an adjustable jacket strip length from 17.5 to 35.0 mm. Reserved strength member stubs are set between 7.0 and 11.0 mm to fit common termination hardware.

Cutting FRP/Steel Members

The machine cleanly cuts FRP and steel wire strength elements while protecting neighboring fibers. Customized cutters are offered for non-standard cross-sections to maintain precision.

  • Automatic waste ejection and sensor start cut idle time.
  • Compact size (L40 × W18 × H18 cm), 50W at 110–220V, and 11 kg weight simplify cell integration.
  • Pneumatic cylinders and PLC/photoelectric control boost reliability and lower maintenance interruptions.
Spec Value Why it matters
Cycle time ~1.5 s (~20/min) Supports high-volume runs
Strip lengths (A) 17.5–35.0 mm Compatible with common connectors
Stub (B) 7.0–11.0 mm Meets strength and termination needs
Power & size 50W @ 110–220V; 40×18×18 cm Easy integration into existing equipment

Using this machine, Shanghai Weiye OFC Equipment standardizes prep so field teams receive drop parts ready for quick installation. The CLX-BPO2 helps our production lines meet volume goals without compromising quality.

Tailored Specifications for Your Network

Shanghai Weiye OFC Equipment configures every order to fit your network requirements and simplify field rollout. We combine focused options with predictable schedules so your teams receive ready-to-install products.

Choose 1 to 4 cores with single-mode or multimode fiber. Options include OS1, OS2, and OM2–OM4 plus G.652D and G.657 variants to align with optics and connector plans.

We Pantone-match sheath colors for fast field ID and consistent asset tags.

Jacket materials, print legends, and branding

Select LSZH, PVC, or PE jackets to suit route and safety requirements. Custom legends/logos aid inventory/warranty tracking.

Put-Ups, Packaging, and Structures

Standard put-ups are 1/2/4 km with tailored reels and packaging to suit storage and handling. Choose bow-type flat or self-supporting designs and steel wire or FRP strength members to fit span and isolation requirements.

Choice Typical Advantage
Length 1 / 2 / 4 km Simpler staging and reels
Jacket LSZH, PE, PVC Indoor/outdoor compatibility
Structure Flat bow / Self-supporting Flexible routing/span

As a supplier, Shanghai Weiye schedules runs to your plan and delivers documentation that lists final specifications for easy on-site QA.

Quality, Test, and Docs

Shanghai Weiye OFC Equipment builds checkpoints into production so every item ships with recorded acceptance data.

High-temperature, salt spray, and vibration laboratory testing

Our lab conducts elevated-temperature exposure, salt spray corrosion, and mechanical vibration to qualify materials and assemblies. These tests simulate field stresses for indoor and outdoor use.

Full Test Reports for Every Reel

Every fiber optic cable includes a 100% test report that records loss, return loss, and key geometry where applicable. Final inspection gates stop nonconforming items before they leave the factory.

Audit Trail and Compliance

Lot/batch records link tests to reels/serials so audits and claims are easy to verify. Documentation uses standard customer templates to speed approvals and inbound inspection.

  • Line checks and final inspection prevent field failures and cut warranty events.
  • QA packages include spec confirmation and formatted data for rapid review.
  • Continuous test trends inform preventive maintenance and raise long-term reliability.
Test Purpose Outcome
High-temperature Material stability Validated heat endurance
Salt-fog Corrosion robustness Qualified for outdoor use
Vibration Resistance to vibration Improved field reliability

Pricing and cost drivers for FTTH drop cable

Budgeting for a drop run starts with fiber and jacket choices and is refined by volume and customization.

Typical prices range broadly—from about $30 to $1,000 per unit—based on fiber grade (G.652/G.657/OM2–OM4), jacket material, length, and design structure.

Material choices, fiber grade, jacket type, and structure

The primary cost drivers are fiber grade, jacket material, and the structural type chosen for deployment.

Self-supporting designs and steel strength elements increase material/labor. Custom sheath colors/logos/legends add setup time and impact pricing on small runs.

Length/Volume/Customization Impact

Longer put-ups and larger volumes lower unit cost. Small quantities often include setup charges and higher per-unit charges.

  • Changeovers and special cutters extend lead time and add cost.
  • Clear RFQs with schedule alignment let Shanghai Weiye OFC Equipment align price quotes to delivery windows.
  • Framework agreements and indexed pricing stabilize budgets over phases.
Factor Price impact Recommendation
Optical grade High impact Balance spec vs. budget
Jacket type Medium impact Compare LSZH vs. PE for total cost
Length/Volume Large Consolidate where possible

Lead times, MOQ, and delivery for the United States

Shanghai Weiye OFC Equipment keeps lead times/logistics clear so planners can align crews and sites. Predictable schedules reduce downtime and help control cost when a rollout is underway.

Scheduling & Capacity Planning

Typical production windows run 4–5 days for orders under 100 km and 7–10 days for orders under 500 km. We plan capacity to track your milestones and to keep deliveries on time.

The service team issues production updates and tracking so installation teams can plan arrivals. For compressed schedules, we hold contingency capacity to accelerate critical-path orders.

Why MOQ Matters

The MOQ is 1 km. This reflects setup needs such as wire and jacket die adjustments that use startup material and generate scrap.

We review your put-ups and staging to select reels to reduce waste/handling. Batch releases can balance inventory with more frequent small-site deliveries.

Installation Scenarios & Readiness

On-site conditions dictate whether a self-supporting aerial, ducted pull, or direct-buried run is the right choice for a project.

Aerial, duct, and direct-buried deployment considerations

For aerial runs, Shanghai Weiye OFC Equipment advises self-supporting designs with correct strength members to manage sag/tension for long-term stability.

Duct installations perform best with low-friction sheaths and crush-resistant builds so pulling does not damage fibers. PE jackets are common for underground and buried paths where moisture resistance matters.

Direct-buried designs require proper depth control per local codes and moisture barriers to protect the fiber core long-term.

Indoor Riser/Plenum & ONT

Indoor riser/plenum routes favor LSZH jackets to meet smoke/flame codes. Flat drop profiles strip clean and present controlled strength stubs for fast ONT terminations.

We advise on steel vs FRP (dielectric) strength members based on bonding requirements, lightning risk, and hardware fit. Standardized line prep shortens install time and reduces scrap.

Scenario Key feature Field note
Aerial Self-supporting, steel or FRP Check tension and messenger hardware
Underground duct Low-friction, crush-resistant Use pull tape and proper lubricant
Direct-buried PE jacket, moisture barrier Follow depth/warning tape codes
Indoor LSZH jacket, tight bend support Maintain bend radius at wall penetrations

Our approach ensures a consistent install experience across indoor outdoor transitions. That leads to fewer callbacks, faster activations, and reliable field performance for your system.

Comprehensive Support & After-Sales

Our team coordinates testing, scheduling, and installation guidance to avoid surprises in deployment.

Shanghai Weiye OFC Equipment offers engineering support from early requirements capture through approved drawings and pilot builds. We provide doc templates and clear install notes so field crews work from the same plan.

After-sales service covers rapid response, root-cause analysis, and corrective actions. All products ship with full reports and traceability to support QA acceptance.

  • 24/7 availability for status and technical support.
  • Warranty with free replacement if any quality problems are confirmed.
  • Schedule coordination for urgent changes or acceleration requests.
  • Configuration control so shipped items match agreed specs consistently.
Support area What we do Benefit
Tech/Eng Spec review & pre-production builds Reduced field issues
QA/Testing Lab trials & 100% test reports Traceable quality
Service Fast replace + RCA Lower downtime

Wrap-Up

Select Shanghai Weiye OFC Equipment for custom drops, quick lead times, and full traceability.

We provide custom FTTH drops that pair material choices with validated manufacturing and lab testing. Every reel ships with a 100% test report and documented trials to support U.S. field acceptance.

A robust production line, including CLX-BPO2 prep assets, cuts variability and shortens turnaround. Our equipment and machines standardize strip/stub lengths so installers see consistent results at turn-up.

From fiber selection to jacket, printing, and packaging, we balance design and cost to extend service life. Dedicated customer support covers scheduling/logistics/after-sales so your deployment stays on plan.

Get in touch with Shanghai Weiye OFC Equipment to align specs, timeline, and volume. We stand behind every shipment with lab validation and responsive support.

Related: How to Maximize the Lifespan of Your Fiber Coloring Machine

Gate Valve Applications in Airport Infrastructure

Cast-Iron Gate Valves: Features, Benefits, and Uses

Could a single, well-made valve cut maintenance time and keep water systems running longer?

I manufacture and supply Cast Iron Gate Valve Manufacturer at Yaxing Valve, and I support their quality and service for U.S. customers. The range is designed for a long service life in municipal and light industrial water systems.

Each unit pairs a sturdy iron body with a machined wedge track and easy handwheel control. The result is dependable shutoff, simple maintenance, and consistent performance in mechanical rooms, fire loops, and distribution networks.

I partner with specifiers to accelerate submittals and provide clear data: diameters, ends, class ratings, and accessory options. My site also keeps account preferences and carts with cookies so repeat orders are simple.

If you need a practical replacement or a cost-effective option for new projects, weigh these cast iron gate valve benefits versus existing hardware to spot life-cycle value and practical fit.

Reliable Flow Control: Why I Trust Yaxing Valve Cast Iron Gate Valves

I personally validate each product at Yaxing Valve, so I can recommend our hardware with confidence for demanding U.S. jobsites.

Industrial performance anchored by a robust cast-iron body

Every valve features a strong cast-iron body that resists load-induced deformation. Metal-to-metal seating and precise machining ensure tight shutoff when customers need it most.

Cast Iron Gate Valve Manufacturer

Flow-optimized design with minimal pressure loss

A streamlined flow path cuts turbulence and pressure drop. That helps pumps run more efficiently and lowers energy use across systems.

  • Dimensions and testing are validated to ANSI norms and internal criteria.
  • I refine stem/wedge/bonnet interfaces to reduce friction and maintain consistent torque over time.
  • I set body thickness targets for durability while keeping weight manageable for installers.
  • Documentation lists tests/standards so purchasing can wrap orders quickly.
Design Feature Benefit Tech Note
Robust iron body High rigidity Dimensional stability verified
Optimized gate geometry Lower pressure loss Improves pump efficiency
Finished stem/handwheel interfaces Smoother operation Consistent torque, long life
Spec documentation Faster spec approval ANSI-referenced reports

Cast Iron Gate Valves—Materials, Design Details, and Key Performance

I outline the body, sealing, and stem choices to make selection and ordering straightforward.

Body/Bonnet/Wedge Materials

I define the material stack-up plainly: a cast iron body and bonnet, a precision-machined wedge, and a metal-to-metal seat interface for dependable isolation across water service and general industry.

Stem and Handwheel Options

I offer non-rising stem and inside screw stems for compact installations. Every thread form and packing scheme is listed in the product details.

Performance Envelope and Standards

I publish qualified pressure and temperature ranges and align end connections to common ANSI standards so engineers can confirm fit quickly.

  • Stem/handwheel interface tuned for steady torque.
  • Geometry and smooth internal surfaces minimize headloss through the gate.
  • Clear series IDs and submittal specs accelerate approvals.
Component Construction Rated Limit Comments
Valve body/bonnet Cast iron Class 125/approx. 150 psi ANSI flange dimensions, welded/bolted options
Gate wedge Precision-machined metal Service temp −20° to 180°F Metal-seat interface; smooth finish
Operating stem Inside-screw / non-rising — Documented thread and packing in datasheet
Series YX-100 and YX-200 2–12 inch range Part numbers simplify bidding

Modern Applications, Install, and Operation

I advise contractors/owners on best-fit placements in today’s water and utility circuits. My goal is to make selection, installation, and operating checks straightforward so crews complete commissioning without callbacks.

Waterworks, building systems, and general industry applications

Use a full-bore unit where low restriction matters — long mains, service feeds, and bypass lines benefit the most.

Where vertical space is constrained, use non-rising or inside-screw stems in mechanical rooms and process loops.

Install best practices

During handling, protect the body, lift at rated points, and avoid stressing flanges. Confirm end alignment before final bolt torquing to prevent leaks and distortion.

Choose media-compatible gaskets, use a cross-torque sequence, and provide supports to prevent sag.

Operation & maintenance notes

Place the handwheel for comfortable reach and confirm smooth movement after packing adjustments.

Perform periodic torque checks under pressure, inspect the wedge and packing, and confirm the pressure/temperature range against your media. Capture tag IDs in your account and link CMMS work orders.

Area Action Timing Outcome
Use-case mapping Use full-bore on mains; inside-screw/NRS in tight spots Design phase Lower headloss; space savings
Handling/installation Use lift points, align ends, torque in sequence Install Prevents flange stress and leaks
Operational checks Verify handwheel feel; test under pressure Startup and routine Consistent operation and shutoff
Recordkeeping Tag units and connect to CMMS/account Ongoing Quicker parts tracking/replacement

Correct handling/commissioning extends service life and keeps Resilient Seated Gate Valve performing and looking like new.

Work with Me at Yaxing Valve to Specify the Right Iron Gate Valve Today

Contact me with your line size, pressure expectations, and flow needs and I will match the exact series and type to your duty range and temperature limits.

My concise checklist speeds approvals: end type, inside-screw vs non-rising, and handwheel orientation. I also capture stem/handwheel and screw details for clear install guidance.

View the images gallery for high-resolution images and a clean gallery layout that shows clearance and operator reach. Create an account so I can save specs, track valves by tag, and link drawings and a one-page PDF for the field.

Ask for a quick quote and I’ll confirm availability, lead times, alternates, and help you complete the order while you view the gallery. I use cookies only to keep your account session and cart ready.

What Is Plastic Mold Fiber Reinforced Molding

Best Practices for Sourcing Injection Molding from China

Well, the major meeting has just concluded. your new product has been approved, the timeline is aggressive, and the budget is… well, let’s just say it’s tight.. Then a voice—perhaps your manager or the CFO—drops the line that gives every project manager a shock: “We should look at sourcing this from China.”

You nod, of course. It makes sense on paper. The potential savings can be massive. But your mind is already racing. You know the rumors, don’t you? The nightmare of defective parts, opaque communication, and delayed, off-spec shipments. It can feel like you’re being asked to walk a tightrope between landing a huge cost win for the company and steering your project straight into a ditch.

However, here’s the reality. Sourcing plastic mold doesn’t have to be a gamble. It’s a project, just like any other. And like any project, it succeeds or fails based on the process you follow. It’s not just about the lowest bid but selecting the best partner and overseeing every step. Forget the horror stories. Here’s a practical playbook to nail it.

China injection molding

Initial Step: Prepare Your Information

Before searching suppliers or opening Alibaba, nail down your requirements. Truthfully, over fifty percent of offshore sourcing issues originate in an unclear project brief. Don’t assume a remote factory can guess your needs. It’s akin to asking someone to price-build “a structure” with no details. You’ll get wildly varied quotes that are useless.

Your RFQ should be bulletproof—clear, detailed, and unambiguous. It’s the cornerstone of your entire effort.

So, what goes in it?

Start with your 3D design files. They’re essential. Use standard formats such as STEP or IGS to ensure compatibility. This is the master blueprint for your part’s geometry.

However, 3D alone won’t cut it. Include precise 2D engineering drawings. This details critical info missing from the 3D file. Examples include tolerances (e.g., ‘25.00±0.05 mm’), material grade, surface finish requirements, and functional callouts. Call out smooth surfaces or precision hole sizes in big, bold notation.

After that, material choice. Avoid generic terms like “Plastic.” Nor just “ABS.” Get precise. Call out SABIC Cycolac MG38 (black), for example. Why so detailed? Because there are thousands of plastic variations. Defining the exact material guarantees the performance and appearance you designed with what is plastic mold.

They can offer alternatives, but you must provide the initial spec.

Lastly, add your business data. What’s your forecasted annual volume (EAU)? They need clarity: is it 1,000 total shots or a million units per annum? The tool design, the number of cavities, and the price per part all hinge on this number.

Finding the Right Supplier

With your RFQ perfected, who will you target? The internet has made the world smaller, but it’s also made it a lot noisier. Finding suppliers is simple; finding quality ones is tough.

Your search will likely start on platforms like Alibaba or Made-in-China.com. These are great for casting a wide net and getting a feel for the landscape. Use them to build a shortlist, not the final list. You’ll want to quickly build a list of maybe 10 to 15 companies that look promising.

However, don’t end your search there. Think about engaging a sourcing agent. True, they charge a fee. But a reputable agent brings pre-screened factories. They bridge language and cultural gaps. For a first-time project, this can be an invaluable safety net. Consider it timeline insurance.

Another classic method? Trade shows. If you can attend, shows such as Chinaplas transform sourcing. Nothing beats a face-to-face conversation. Inspect prototypes, interview engineers, and sense their capabilities. Also, leverage the tried-and-true referral network. Tap your professional contacts. Peer endorsements carry huge weight.

Shortlisting Serious Suppliers

With your RFQ dispatched to dozens of firms, the quotes will start trickling in. Some prices will undercut logic, others will shock you. Now, sift through and shortlist 2–3 reliable candidates.

How do you do that? It involves both metrics and gut feel.

Begin with responsiveness. Are their replies prompt and clear? Do they communicate effectively in English? But the key: do they probe your RFQ? The best firms will question and suggest. “Have you considered adding a draft angle here to improve ejection?” or “We see your tolerance requirement here; our CMM can verify that, but it will add to the inspection time. Is that acceptable?” Consider that a big green light. It shows they’re engaged and experienced. A supplier who just says “No problem” to everything is a walking red flag.

Afterward, verify their technical arsenal. Get their tooling inventory. Review examples of parts akin to your design. If you’re making a large, complex housing, you don’t want a shop that specializes in tiny gears.

Finally, inspect the factory. You can’t skip this. You would never hire a critical employee without an interview, so why would you send tens of thousands of dollars for a tool to a company you’ve never truly vetted? Either visit in person or engage a local audit service. They’ll send a local inspector to the factory for a day. They confirm legitimacy, audit ISO 9001, inspect equipment condition, and gauge the facility. That small investment can save you thousands.

Converting Digital Designs into Molded Parts

You’ve selected your partner. you’ve negotiated the price and payment terms—a common structure is 50% of the tooling cost upfront to begin work, and the final 50% after you approve the first samples. Now the process kicks off.

Initially, expect a DFM report. DFM stands for Design for Manufacturability. This is your supplier’s formal feedback on your part design. They’ll flag thick sections prone to sink, sharp edges that stress, or insufficient draft. A thorough DFM is a sign of a professional operation. It’s a collaboration. Together, you tweak the design for best manufacturability.

With DFM sign-off, toolmaking begins. A few weeks later, you’ll get an email that will make your heart beat a little faster: “T1 samples have shipped.” These are the very first parts off the new tool. It’s your first real test.

Be prepared: T1 samples are almost never perfect. It’s par for the course. You’ll find minor defects, off-spec dimensions, or finish issues. You critique, they refine, and T2 plastic mold company parts arrive. It could require several iterations. The key for you, as the project manager, is to have this iteration loop built into your timeline from the start.

Finally, a flawless part arrives. It meets every dimension, the finish is flawless, and it functions exactly as intended. This becomes the “golden sample.” You ratify it, and it becomes the quality yardstick for production.

Crossing the Finish Line

Receiving the golden sample seems like victory, but you’re not done. Now you’re entering the mass production phase. How can you keep part #10,000 matching your golden sample?

Put a strong QC process in place. This often involves a pre-shipment inspection. Use a third-party inspector again. For a few hundred dollars, they will go to the factory, randomly pull a statistically significant number of parts from your finished production run, and inspect them against your 2D drawing and the golden sample. They’ll send you a detailed report with photos and measurements. Only after you approve this report do you authorize the shipment and send the final payment. This simple step prevents you from receiving a container full of scrap metal.

Finally, think about logistics. Clarify your Incoterms. Is your price FOB (Free On Board), meaning the supplier’s responsibility ends when the goods are loaded onto the ship in China? Or EXW, where you handle everything from their gate? These choices hugely affect landed cost.

Overseas sourcing is a marathon. It relies on partnership-building. View them as allies, not vendors. Clear communication, mutual respect, and a solid process are your keys to success. Certainly, it’s complex. However, armed with this guide, you’ll secure savings and keep high standards intact. You’re ready.